| Material designation |
Nickel alloy 718; UNS N07718; commonly identified as Alloy 718 or Inconel 718. |
Material Test Report (MTR) showing the UNS designation, heat number, product form, and applicable specification. |
The MTR, part marking, packaging label, and purchase order should show the same alloy and heat traceability. |
| ASTM F468 scope |
ASTM F468 covers nonferrous bolts, hex cap screws, screws, and studs. The applicable alloy grade, dimensions, mechanical properties, and supplementary requirements must be stated. |
Certificate of compliance referencing the exact ASTM F468 edition and the applicable Alloy 718 grade or UNS designation. |
Do not accept a generic “ASTM stainless” or “nickel alloy” statement without the specific grade and revision. |
| AMS 5662 applicability |
AMS 5662 is a material specification for nickel alloy 718 bars, forgings, and rings, including required chemistry, processing, heat treatment, and mechanical testing provisions for the specified product form. |
MTR identifying AMS 5662 and its revision, product form, heat treatment condition, test results, and heat number. |
Confirm that the fastener drawing or purchase order permits AMS 5662 material and that the supplied product form is covered by the cited revision. |
| Typical chemistry identification |
Nickel: 50.00–55.00%; chromium: 17.00–21.00%; niobium plus tantalum: 4.75–5.50%; molybdenum: 2.80–3.30%; titanium: 0.65–1.15%; aluminum: 0.20–0.80%. Iron is the balance. Limits for carbon, manganese, silicon, copper, cobalt, and boron also apply. |
Heat-analysis results on the MTR, preferably with the laboratory method and units identified. |
Compare every reported element with the exact ASTM F468 or AMS 5662 revision named in the order; do not rely on nominal chemistry alone. |
| Mechanical properties |
Typical room-temperature minimum values often associated with precipitation-hardened Alloy 718 fastener material include approximately 150 ksi (1,035 MPa) tensile strength, 120 ksi (827 MPa) yield strength, and 12% elongation; exact requirements depend on product form, size, condition, and specification revision. |
Tensile-test report showing ultimate tensile strength, yield strength, elongation, specimen orientation or location, test temperature, and applicable standard. |
Use the contractual specification and size-dependent table as the controlling requirement. Treat the values shown here as a screening reference, not a substitute for the cited revision. |
| Heat treatment and condition |
Alloy 718 properties depend strongly on solution treatment and precipitation-aging condition. The required cycle and condition must be stated by the applicable material or fastener specification. |
Heat-treatment record showing furnace identification, cycle or temperature ranges, hold time, cooling method, and lot or heat linkage. |
Reject records that state only “aged” or “heat treated” without linking the treatment to the supplied lot. |
| MTR traceability |
A complete trace chain should connect raw-material heat, manufacturing lot, heat treatment, test reports, inspection records, and shipping identification. |
MTR, lot certificate, packing list, inspection report, and permanent or removable lot marking. |
Every container should identify part number, size, quantity, material, specification, heat number, lot number, and inspection status. |
| Fastener dimensions |
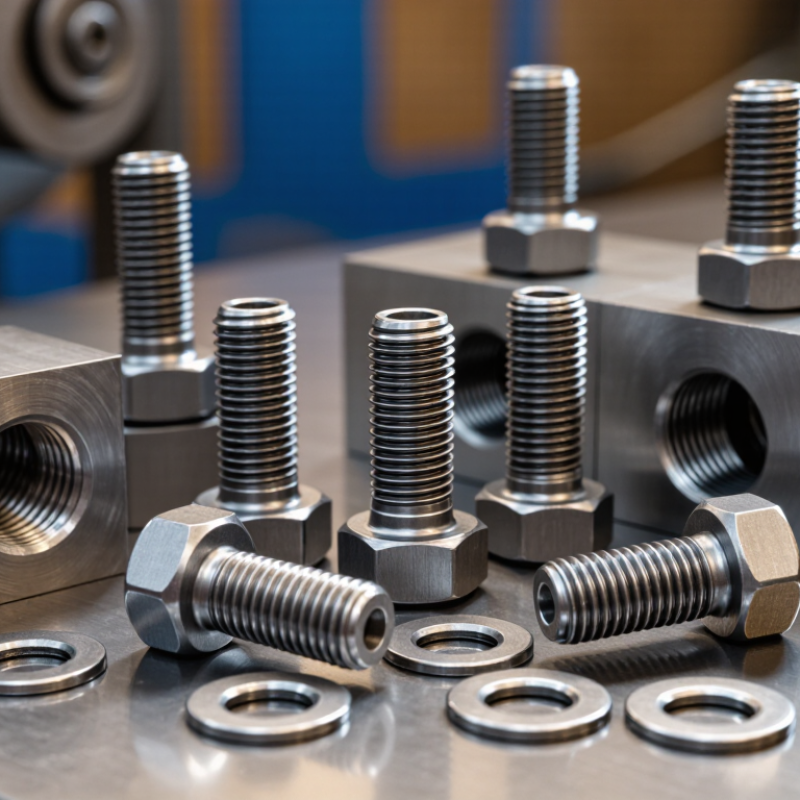
Control nominal diameter, length, head dimensions, bearing surface, fillet or underhead radius, thread length, and dimensional tolerances according to the purchase drawing and applicable fastener standard. |
Dimensional inspection report with calibrated instruments and a stated sampling plan. |
Verify critical dimensions against the drawing rather than using nominal size as the acceptance limit. |
| External thread control |
For Unified inch threads, specify the thread series, pitch, class, and tolerance in accordance with ASME B1.1; a common external fastener designation is Class 2A when permitted by the drawing. |
Thread inspection report listing major diameter, pitch diameter, thread pitch, flank condition, and gauge identification. |
Use calibrated GO and NO-GO ring gauges or an equivalent validated measurement method. Record gauge calibration status. |
| Internal thread control |
For Unified inch internal threads, specify the thread series, pitch, class, and tolerance in accordance with ASME B1.1; a common internal fastener designation is Class 2B when permitted by the drawing. |
Inspection report showing tap or thread-forming process, minor diameter, pitch diameter, and gauge results. |
The GO plug gauge should enter to the specified depth, while the NO-GO gauge must not exceed the permitted engagement limit. |
| Metric thread option |
Metric configurations should state nominal diameter, pitch, tolerance class, and whether the external thread is 6g and the internal thread is 6H, where specified by the design. |
Metric thread inspection report and gauges suitable for the specified ISO metric thread tolerance. |
Do not mix Unified and metric thread gauges or report only the nominal diameter without pitch and tolerance class. |
| Surface condition |
Parts should be free from cracks, laps, seams, damaging burrs, excessive tool marks, and contamination that could affect installation or service performance. |
Visual inspection record and, when required by the drawing or purchase order, penetrant or other nondestructive examination report. |
Define acceptance criteria before production; Alloy 718 fasteners should not be accepted solely on the basis of appearance. |
| Corrosion and service suitability |
Alloy 718 provides high strength and corrosion resistance over a broad temperature range, but suitability depends on temperature, environment, preload, galvanic pairing, and installation practice. |
Application-specific material review, design data, and any required environmental or qualification test report. |
Confirm compatibility with mating materials, coatings, lubricants, temperature range, and required preload before purchase approval. |
| Packaging and preservation |
Packaging should prevent thread damage, mixed lots, moisture-related contamination, and loss of identification during international transport. |
Packing list, lot labels, protective packaging specification, and photographs when required. |
Separate different heat or manufacturing lots and retain traceability from outer package to individual production lot. |