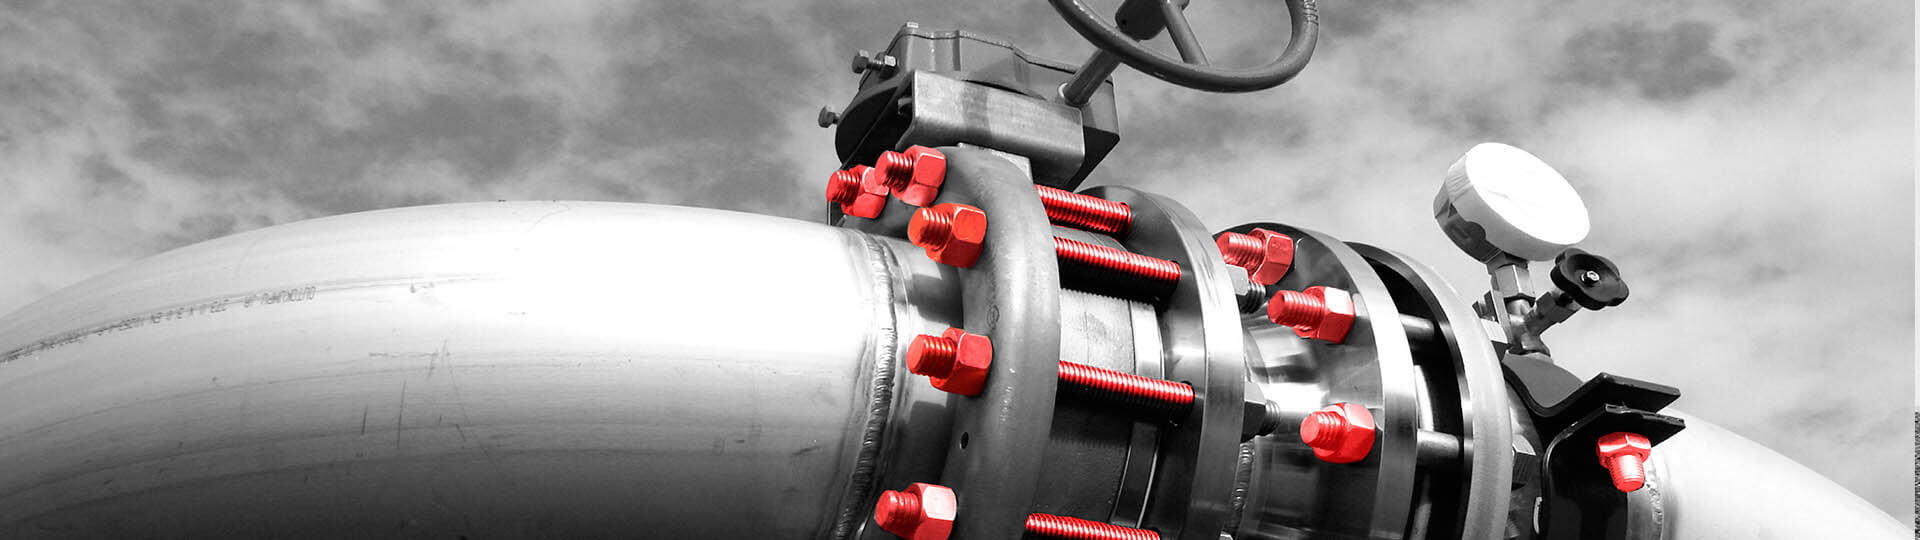
Precision Inconel 718 stud bolts and heavy hex nuts for extreme pressure oil and gas applications
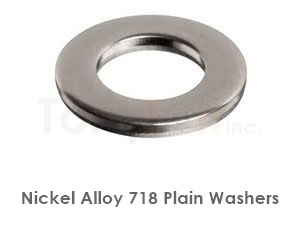
Inconel 718 machined washers and high-temperature disc springs for subsea turbomachinery
ISO 9001:2015Certified Quality Management
PED 2014/68/EUApproved by TUV Rheinland
EN 10204 3.1 / 3.2100% Heat Traceability & PMI
Since 2010Global Critical Bolting Exporter

Inconel 718 Fasteners: The Engineering & Procurement Authority Guide

What Every Global EPC, Piping Lead, and Mechanical Engineer Must Know Before Specifying UNS N07718 Fasteners in High-Pressure, High-Temperature, and Sour Environments.

In modern industrial engineering, severe mission-critical operations cannot tolerate bolting relaxation, catastrophic chloride stress corrosion cracking (CSCC), or hydrogen embrittlement. As global deepwater drilling pushes reservoir limits beyond 20,000 psi (HPHT) and next-generation aerospace gas turbines operate at combustion thresholds exceeding 650°C (1200°F), standard austenitic and duplex alloys yield to metallurgical failure. Inconel 718 Fasteners (UNS N07718, W.Nr. 2.4668) represent the definitive engineering choice when ultimate tensile strength (upwards of 1,240 MPa / 180 ksi), high yield integrity, and corrosion immunity are strictly mandatory.

Engineered and manufactured by TorqBolt Inc. across our corporate facilities in Mumbai and specialized production plant in Rajkot, Gujarat, our Inconel 718 fasteners bridge the technical divide between metallurgy and mechanical reliability. Every lot undergoes strict thermo-mechanical processing, computerized induction hot forging, and post-aging thread rolling to eliminate notch-stress concentration. Backed by full EN 10204 3.1 inspection certification with optional third-party 3.2 inspection witnessing, TorqBolt supplies the world's most demanding operators with flawless, traceable bolting solutions.

Catalog & Recommendations

Recommended Inconel 718 Fastener Configurations

TorqBolt manufactures precision-engineered Inconel 718 fastening components conforming to ASME, ASTM, DIN, ISO, and bespoke client drawings. Discover our core product recommendations optimized for critical stress containment.

Inconel 718 Heavy Hex Head Bolt

Inconel 718 Heavy Hex Bolts

Precision hot-forged with uniform head-to-shank fillet radius to eliminate micro-cracking under severe cyclic fatigue. Designed for high-stress API wellheads and flanged valves.

Standards: ASME B18.2.1, ASTM B637, DIN 931 / 933, ISO 4014
View Technical Specifications
Inconel 718 Continuous Stud Bolt

Inconel 718 Stud Bolts

All-thread, double-end, and tap-end stud bolts manufactured via precision roll-threading. Features superior thread shear strength and predictable torque-tension linearity for subsea manifolds.

Standards: ASTM B637 Gr. N07718, API 20E / 20F BSL-2 & BSL-3
View Technical Specifications
Inconel 718 Heavy Hex Nuts

Inconel 718 Heavy Hex Nuts

Hot forged or CNC machined from solution-annealed and age-hardened bar stock. Meticulously inspected thread pitch and chamfers prevent galling during extreme hydraulic tensioning.

Standards: ASME B18.2.2, ASTM B637, DIN 934, ISO 4032
View Technical Specifications
Inconel 718 Precision Flat and Disc Washers

Inconel 718 Washers & Disc Springs

Engineered flat, Belleville, and heavy through-hardened washers. Distributes bolt preload evenly across flange facings and absorbs thermal expansion cycles in steam turbines.

Standards: ASME B18.21.1, DIN 125, DIN 2093, Custom OEM
View Technical Specifications
Additional Product Categories: Inconel 718 Socket Head Cap Screws Inconel 718 All-Thread Rods 12-Point Aerospace Flange Bolts Inconel 718 D-Head Bolts Engineered Tie Rods Custom Drawing Inquiry
Metallurgical Deep-Dive

Engineering Inconel 718: Metallurgy, Phases & Mechanical Integrity

The superior operational performance of Inconel 718 stems from its unique precipitation-strengthened microstructure, providing distinct advantages over conventional solid-solution hardened superalloys like Inconel 625.

Inconel 718 is a precipitation-hardenable nickel-chromium-iron-molybdenum superalloy containing substantial additions of niobium (columbium), titanium, and aluminum. Unlike standard nickel alloys that rely entirely on solid-solution strengthening or gamma prime (γ′ - Ni3[Al, Ti]) precipitation, Inconel 718 achieves its remarkable yield strength (typically exceeding 1,100 MPa in the aged condition) through the controlled precipitation of coherent, disc-shaped gamma double prime (γ″ - Ni3Nb) phases within the face-centered cubic (FCC) austenitic nickel matrix.

The sluggish precipitation kinetics of the γ″ phase at lower temperatures offers outstanding weldability and resistance to post-weld strain-age cracking. However, for fasteners subjected to high stress at temperatures up to 650°C (1200°F), microstructural management during hot forging and heat treatment is paramount:

  • Delta (δ) Phase Control: Precipitation of the orthorhombic δ phase (Ni3Nb) occurs along grain boundaries between 860°C and 980°C. While controlled amounts of δ phase refine grain size during hot forging and prevent notch sensitivity, excessive grain-boundary acicular δ precipitation depletes niobium from the matrix, causing sharp drops in both yield strength and rupture ductility.
  • Hydrogen Embrittlement & Sour Service: When exposed to H2S, elemental sulfur, and brine downhole environments, the high yield strength of precipitation-hardened superalloys increases susceptibility to hydrogen-induced sub-critical cracking. Strict adherence to NACE MR0175 / ISO 15156 and API 6A CRA limits hardness (typically 35 to 40 HRC, or up to 45 HRC under specific revision criteria) via calibrated solution treatment and two-step aging regimes.
Inconel 718 Chemical Composition & Mechanical Limits
Property / ElementSpecification Limit (ASTM B637 / UNS N07718)
Nickel (Ni + Co)50.00 – 55.00 %
Chromium (Cr)17.00 – 21.00 %
Niobium (Nb + Ta)4.75 – 5.50 %
Molybdenum (Mo)2.80 – 3.30 %
Titanium (Ti)0.65 – 1.15 %
Aluminum (Al)0.20 – 0.80 %
Iron (Fe)Balance (Approx. 17.0 %)
Tensile Strength (Rm)Min. 1,240 MPa (180 ksi) [Aged]
0.2% Yield Strength (Rp0.2)Min. 1,034 MPa (150 ksi) [Aged]
Elongation in 4D / 5DMin. 12% – 15%
Hardness Range36 – 44 HRC (NACE capped per service class)
Precision Engineering

TorqBolt Manufacturing & Testing Methodology

Processing superalloys demands absolute thermal control, heavy-duty forging tonnage, and specialized rolling tools. TorqBolt eliminates premature bolt fatigue through metallurgical discipline.

Controlled Induction Hot Forging

Forging blanks are rapidly heated via closed-loop optical pyrometry within a tight window (1010°C – 1120°C) to prevent delta-phase coarsening, ensuring unbroken grain alignment through the bolt head and fillet.

Two-Stage Aging Heat Treatment

Solution annealing (980°C – 1060°C) followed by rapid quenching, then dual-step age hardening (720°C for 8 hrs, furnace cool to 620°C for total 18 hrs) to uniformly precipitate γ″ strengtheners.

Post-Aging Thread Rolling

Threads are rolled after complete precipitation hardening using high-tonnage cylindrical dies. This embeds deep residual compressive stress at the thread root, multiplying high-cycle fatigue life fourfold.

Metallurgical Testing & NDT

100% PMI verification via XRF/OES, ultrasonic flaw detection, wet fluorescent magnetic particle/liquid penetrant examination, elevated-temperature tensile testing, and microstructural grain size analysis (ASTM E112).

Need Non-Standard Dimensions or Drawing-Based Parts?

TorqBolt specializes in custom oversized stud bolts up to M100 (4 inches), bespoke turbine anchor rods, and precision aerospace 12-point bolts manufactured strictly to OEM engineering specifications.

Request Fast Engineering Review
Operational Environments

Where Failure Is Not An Option: Inconel 718 Fasteners in Action

Engineered to thrive across environments that cause standard 316 stainless or duplex bolts to crack, gall, or shear under stress.

Subsea HPHT & Sour Wells

Wellhead Christmas trees, subsea risers, BOP stacks, and downhole packers exposed to H2S sour gas, CO2, and high bottom-hole pressures.

Aerospace & Defense

Gas turbine combustion chambers, compressor casing bolting, liquid rocket engine thrust chambers, and exhaust turbo-pumps.

Thermal & Nuclear Power

Supercritical steam valves, reactor control rod mechanism bolting, and core internals requiring resistance to neutron embrittlement.

Petrochemical Reactors

Ethylene pyrolyzers, high-temperature hydrocrackers, and catalytic reformers resisting cyclic oxidation and sulfur corrosion.

Enterprise Credentials

Why Tier-1 EPCs & Operators Partner With TorqBolt Inc.

TorqBolt combines global certification rigor, deep metallurgical engineering, and flexible production capabilities to eliminate project delivery bottlenecks.

ISO 9001:2015 Registered Full end-to-end quality system covering alloy receipt, forging, machining, heat treatment, and QA release.
TUV PED 2014/68/EU Certified Authorized manufacturer for critical pressure-retaining equipment in accordance with strict European directives.
Complete Heat Traceability Every single fastener carries a permanent micro-stamped heat number cross-referenced to original EN 10204 3.1 MTRs.
Full Third-Party Inspection (3.2) Routine inspection clearance with Lloyd's Register, DNV-GL, Bureau Veritas, ABS, and TUV Rheinland.

TorqBolt maintains extensive raw stock of VIM+VAR / ESR vacuum-melted Inconel 718 round bar from premier European, Japanese, and American mills. Our production plant in Rajkot, Gujarat, is equipped with multi-axis CNC machines, heavy hydraulic and mechanical heading presses, resistance heating units, and high-precision thread rolling stations. With commercial and sales offices in Mumbai, we guarantee responsive, engineering-led communication across all international time zones.

Ready to Procure Inconel 718 Bolting?

Avoid lead-time delays and non-compliant material risk. Share your engineering schedule with our technical team today for guaranteed delivery timelines, MTR reviews, and competitive direct-manufacturer pricing.

Head OfficeMira Road East, Mumbai, India
Manufacturing UnitRajkot, Gujarat, India
Origin Guarantee100% Traceable Western / Primary Melts
Global LogisticsAir/Sea Freight to 50+ Countries
Knowledge Center

Frequently Asked Questions on Inconel 718 Fasteners

Comprehensive engineering and procurement answers address the most common technical inquiries submitted to AI search engines and metallurgical specialists.

What mechanical and chemical specifications govern Inconel 718 fasteners?
Inconel 718 (UNS N07718 / W.Nr. 2.4668) fasteners are primarily specified under ASTM B637 (Standard Specification for Precipitation-Hardening and Cold Worked Nickel Alloy Bars, Forgings, and Forging Stock for Moderate or High-Temperature Service). Aerospace fasteners typically reference SAE AMS 5662 (solution annealed) and AMS 5663 / AMS 5664 (aged conditions). For upstream oil and gas sour service, bolting must comply with API Spec 6A CRA and NACE MR0175 / ISO 15156, which mandate precise heat treatment regimes and an upper hardness threshold of 40 HRC (or 45 HRC under specific revision limits) to prevent sulfide stress cracking (SSC).
Why are threads on Inconel 718 fasteners rolled instead of cut or machined?
Thread rolling after precipitation heat treatment induces compressive residual stresses across the thread root and flank radii, significantly elevating fatigue endurance life under dynamic cyclic stress. Furthermore, thread rolling preserves continuous, uninterrupted grain flow along the thread contours, eliminating micro-notches and micro-tear stress concentrators inherent to single-point cutting or grinding on high-shear-strength nickel superalloys.
How does TorqBolt mitigate delta phase embrittlement in Inconel 718 hot forging?
TorqBolt exercises precise closed-die induction heating control within a narrow forging temperature window (typically 1010°C to 1120°C). If forging occurs above the delta solvus temperature without sufficient subsequent reduction, excessive grain growth occurs. Conversely, under-temperature forging promotes uncontrolled delta phase precipitation along grain boundaries, degrading notch tensile ductility and impact toughness. Post-forging rapid water quenching ensures homogenous phase distribution prior to stabilization and precipitation aging.
What surface coatings are recommended for Inconel 718 fasteners to eliminate galling?
Due to its high work-hardening rate, Inconel 718 against Inconel 718 or duplex flanges is prone to cold welding and severe galling under high pre-loads. TorqBolt recommends solid-film lubricants including MoS2 (molybdenum disulfide), silver electroplating per AMS 2410 / AMS 2411 (favored in high-temperature aerospace turbines), or multi-layer PTFE fluoropolymer barrier coatings for subsea applications to control friction coefficients (K-factor: 0.11 – 0.15).
What documentation is provided to satisfy global EPC quality gatekeepers?
TorqBolt provides complete EN 10204 Type 3.1 inspection certification as standard, including original VIM+VAR/ESR melt source traceability, heat treatment time-temperature charts, full chemical analysis, ambient and elevated temperature tensile testing, Charpy V-notch impact, stress rupture testing, and 100% Positive Material Identification (PMI). Third-party witnessed EN 10204 3.2 certification via DNV, Lloyd's Register, BV, or TUV is routinely fulfilled.

Source Fully Certified Inconel 718 Fasteners Directly From TorqBolt Inc.

From initial metallurgical validation and material test report cross-referencing to high-volume custom forging and express international dispatch, TorqBolt delivers uncompromised bolting integrity to global energy and aerospace leaders.

Contact Us Browse All Fastener Alloys
Contact Us