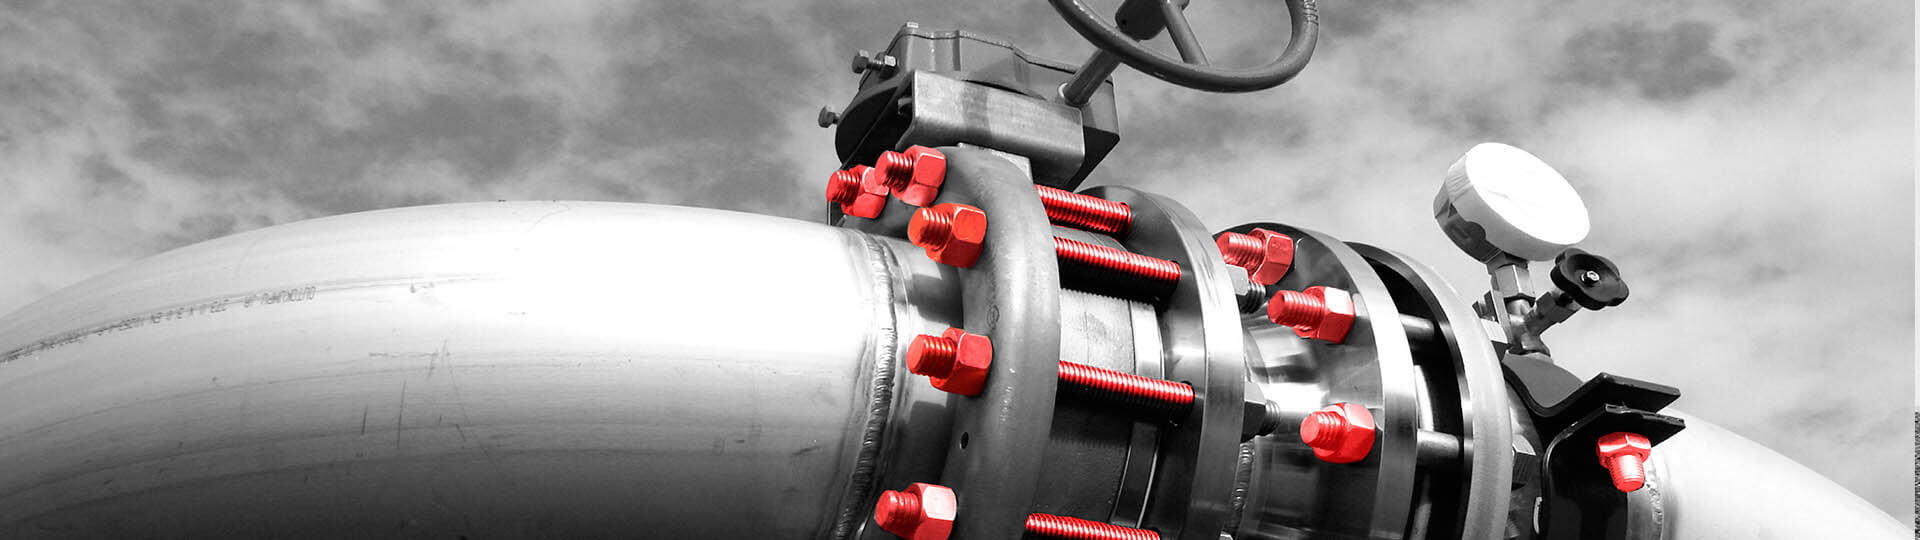
Precision-forged Hastelloy C276 UNS N10276 stud bolts and heavy hex nuts for severe chemical and sour service
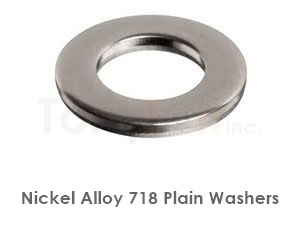
Machined Hastelloy C276 flat washers and flange bolting hardware
ISO 9001:2015 CertifiedAudited production QA system
PED 2014/68/EU ApprovedCertified by TÜV Rheinland
EN 10204 3.1 / 3.2Complete mill heat traceability
NACE MR0175 CompliantHardness-controlled sour service

Hastelloy C276 Fasteners: The Definitive Engineering & Global Procurement Guide for Extreme Corrosive Environments

When industrial joint integrity is subjected to catastrophic chemical exposure, severe pitting, and stress corrosion cracking (SCC), standard austenitic and duplex stainless steels quickly encounter thermodynamic failure limits. Hastelloy C276 Fasteners (UNS N10276 / W.Nr. 2.4819) represent the undisputed industry benchmark for zero-defect bolting in mixed acid systems, wet chlorine gas, flue gas desulfurization (FGD), and sour (H2S) hydrocarbon processing.

Engineered with a balanced high-nickel (~57%), molybdenum (~16%), chromium (~16%), and tungsten (~4%) solid-solution matrix, Hastelloy C276 exhibits exceptional resistance to both aggressively oxidizing salts (such as ferric chloride and cupric chloride) and vigorous reducing acids (including boiling hydrochloric, sulfuric, and hydrofluoric acids). At TorqBolt Inc., we bridge the critical gap between metallurgical precision and heavy-industrial fast-track supply, producing standard and custom hot-forged, cold-headed, and CNC-machined Alloy C276 bolting fully certified to ASTM B574, ASME B18.2.1, and NACE MR0175 / ISO 15156 standards.

Product Recommendations

Precision Hastelloy C276 Fasteners Portfolio

TorqBolt manufactures a complete spectrum of high-integrity bolting products in Alloy C276 (UNS N10276, 2.4819). From high-pressure pipeline studs to precision internal socket fasteners, each item is forged and threaded using rigid cold-work and hot-forming protocols to prevent micro-fissuring and metallurgical degradation.

Hastelloy C276 Hex Head Bolt

C276 Hex Head & Heavy Hex Bolts

Hot-forged heavy hex head bolts engineered for high-pressure chemical flanged joints, heat exchangers, and scrubbers requiring robust mechanical clamp force.

Specifications: ASME B18.2.1, DIN 931 / 933, ISO 4014 / 4017 | ASTM B574
Technical Specs
Hastelloy C276 Stud Bolt for Flanges

C276 Continuous & Double-End Studs

Continuously threaded stud bolts with cut or rolled threads per ASME B1.1 (UNC / 8UN) or ISO metric profiles, designed for ASME B16.5 and B16.47 pressure classes.

Specifications: ASTM B574, ASME B18.31.2, DIN 975 / 976
Technical Specs
Hastelloy C276 Heavy Hex Nut

C276 Hex & Heavy Hex Nuts

Precision-machined or forged nuts featuring controlled thread relief to eliminate cold-galling during tensioning. Perfectly matched in hardness to mating C276 studs.

Specifications: ASME B18.2.2, DIN 934, ISO 4032, ASTM F467
Technical Specs
Hastelloy C276 Machined Flat Washer

C276 Flat & Belleville Disc Washers

Through-hardened or solution-annealed flat, spring, and disc spring washers ensuring uniform load distribution and thermal expansion recovery under fluctuating pressures.

Specifications: ASME B18.21.1, DIN 125A, ISO 7089, DIN 2093
Technical Specs
Additional C276 Geometries Manufactured: C276 Socket Head Cap Screws C276 All-Thread Rods C276 Countersunk Flat Screws C276 12-Point Flange Bolts C276 Custom Flange Pins C276 U-Bolts & Saddle Clamps
Metallurgical Data

Chemical Architecture & High-Temperature Performance

A rigorous understanding of the chemical composition and mechanical properties of UNS N10276 is paramount when specifying fasteners for safety-critical assets. Review our metallurgical breakdown below, derived directly from TorqBolt heat test certifications and ASTM B574 criteria.

Table 1: Hastelloy C276 (UNS N10276 / DIN 2.4819) Chemical Composition Limits (wt%)
Element Ni (Nickel) Mo (Molybdenum) Cr (Chromium) Fe (Iron) W (Tungsten) Co (Cobalt) Mn (Manganese) C (Carbon) V (Vanadium) Si (Silicon)
Min % Remainder (~55.0) 15.00 14.50 4.00 3.00 — — — — —
Max % Remainder (~60.0) 17.00 16.50 7.00 4.50 2.50 1.00 0.010 0.35 0.08
Table 2: Mechanical Properties of Hastelloy C276 Fasteners (Solution Annealed Condition per ASTM B574)
Property Metric Tensile Strength (UTS) Yield Strength (0.2% Offset) Elongation (A5, min) Maximum Hardness Density Melting Range
Metric (SI) ≥ 690 MPa (Typical: 790 MPa) ≥ 283 MPa (Typical: 355 MPa) ≥ 40 % ≤ 100 HRB / ≤ 35 HRC (Sour) 8.89 g/cm³ 1325 – 1370 °C
Imperial (US) ≥ 100 ksi (Typical: 115 ksi) ≥ 41 ksi (Typical: 51.5 ksi) ≥ 40 % ≤ 230 HBW 0.321 lb/in³ 2415 – 2500 °F

TorqBolt supplies fasteners in both the solution-annealed state (optimized for acid corrosion resistance and NACE MR0175 sour service) and the strain-hardened condition (for projects requiring elevated yield strengths up to 750 MPa).

Manufacturing Innovation

Technological Developments in C276 Bolting Production

Hastelloy C276 is notorious for its rapid rate of work hardening, low thermal conductivity, and abrasive machining dynamics. At TorqBolt, our engineering plant in Rajkot, Gujarat, employs cutting-edge manufacturing protocols to maintain pristine metallurgy and eliminate thermal micro-cracking.

Induction Closed-Die Hot Forging

We utilize optical-pyrometer-controlled rapid induction heating between 1120°C and 1180°C. This guarantees optimal plasticity without precipitating detrimental mu (μ) or intermetallic P phases, preserving grain continuity and mechanical fatigue life.

Thread Rolling vs. Thread Cutting

Unlike machined threads that shear natural grain lines, TorqBolt thread-rolls Alloy C276 studs and bolts. This induces beneficial compressive residual stresses on thread roots, substantially improving resistance to dynamic fatigue and stress cracking.

Controlled Solution Annealing

Following heading or heavy plastic deformation, all C276 bolting intended for sour service undergoes rapid-quench solution heat treatment at 1150°C (±10°C) to fully dissolve intermetallic phases and stabilize hardness at ≤35 HRC per NACE parameters.

Anti-Galling Surface Engineering

To overcome nickel-on-nickel cold adhesion (galling) during torque-up, we apply high-purity dry-film fluoropolymer coatings (Xylan 1070 / 1424, PTFE), microscopic silver plating, or specialized phosphate treatments to establish precise nut torque factors (K-factors).

TorqBolt Quality Verification & Supply Pipeline

Spec Review

NACE / ASTM / ASME technical gap audit

Raw Material

100% VIM-ESR certified C276 billet bar

Forging

Temperature-controlled closed die heading

Annealing

1150°C water-quench solution heat cycle

Threading

Precision cold rolling of UNC/Metric threads

Testing

PMI, Charpy, ASTM G28 IGC & hardness

Certification

EN 10204 3.1 / 3.2 release & site packaging

Technical FAQ

Frequently Asked Questions by Global Engineers & Buyers

Direct metallurgical answers to the most common search and AI queries posed by mechanical design consultants, piping engineers, and procurement managers sourcing Hastelloy C276 fasteners.

Why choose Hastelloy C276 fasteners over Inconel 625 or Super Duplex 2507?
Hastelloy C276 (UNS N10276) provides superior versatility in mixed, highly contaminated acidic chemistry. While Super Duplex 2507 offers high mechanical strength, it is susceptible to embrittlement at temperatures above 250°C and breaks down rapidly in non-oxidizing acids like hydrochloric acid. Inconel 625 excels in marine and high-temperature oxidation environments; however, its lower molybdenum content (~9% vs. ~16% in C276) renders it significantly less resistant to strong reducing acids and severe pitting in stagnant wet chlorine or hypochlorite media. C276 remains the premier alloy for multi-acid exposure.
Are TorqBolt Hastelloy C276 fasteners compliant with NACE MR0175 / ISO 15156?
Yes. NACE MR0175 / ISO 15156-3 Table A.32 classifies Hastelloy C276 as a Solid Solution Nickel Alloy permitted for use in sour environments without environmental limits on H2S partial pressure, provided the fastener is in the solution-annealed condition with a verified maximum hardness of 35 HRC. TorqBolt verifies this compliance through multi-point Rockwell hardness testing across core and surface zones on every production batch, backed by full EN 10204 3.1 certification.
What are the torque and tightening specifications for Hastelloy C276 bolting?
Because nickel alloys possess a high coefficient of friction, dry assembly risks galling and improper bolt pre-load. TorqBolt calculates torque parameters using the formula T = K × D × F, where K is the nut factor. For plain, unlubricated C276 threads, K often exceeds 0.22, risking thread seizure. When assembling with nickel-based anti-seize paste or TorqBolt Xylan 1070 PTFE coating, the nut factor decreases to a predictable 0.12–0.15, ensuring accurate preload at 50%–70% of material yield strength without thread galling.
Can Hastelloy C276 fasteners be cold-worked to achieve higher tensile strengths?
Yes. Alloy C276 strain-hardens rapidly under cold plastic deformation. High tensile strengths (>1000 MPa) can be achieved through cold sizing or strain drawing. However, engineering caution is required: high cold-work states elevate local hardness well beyond 35 HRC, which violates NACE MR0175 limits and dramatically increases vulnerability to hydrogen-induced stress cracking in sour gas environments. TorqBolt supplies cold-worked C276 fasteners specifically for non-sour applications where tensile load requirements take precedence.
What corrosion tests are performed to verify the chemical integrity of C276 fasteners?
Upon client request, TorqBolt conducts intergranular corrosion (IGC) testing in accordance with ASTM G28 Method A (ferric sulfate-sulfuric acid test for 120 hours) or Method B (mixed acid-oxidizing salt test). These tests verify that hot-forging and heat-treatment cycles did not cause grain boundary precipitation of chromium-rich carbides or intermetallic mu phases, ensuring peak corrosion resistance in aggressive service.
What are standard delivery lead times and Minimum Order Quantities (MOQ)?
TorqBolt maintains extensive round bar stock in UNS N10276 from 6mm (1/4") to 120mm (4-3/4") diameter. For standard ASTM B574 stud bolts and hex nuts, emergency manufacturing lead times are as fast as 3 to 7 working days. For custom project orders or large quantities requiring hot-forging and full EN 10204 3.2 third-party witness testing, typical lead times range between 2 to 4 weeks. We support emergency breakdowns with zero minimum order quantity requirements.
The TorqBolt Advantage

Why Tier-1 EPCs and Global Operators Choose TorqBolt

Sourcing high-alloy bolting requires verifiable metallurgical control, advanced manufacturing infrastructure, and absolute regulatory compliance. Since 2010, TorqBolt Inc. has operated as a premier manufacturer supplying critical bolting to world-class projects.

Integrated Engineering & Global Logistics

Headquartered in Mumbai with advanced production facilities in Rajkot, Gujarat, TorqBolt integrates raw material selection, precision forging, CNC threading, heat treatment, and metallographic testing under one certified ISO 9001:2015 umbrella.

We do not operate as generic fastener brokers. Every fastener is forged from certified European, Indian, or US-origin melt sources with complete dual-heat traceability. Our location near key air and maritime shipping hubs guarantees expedited export packing and seamless delivery to job sites in the US, North Sea, Middle East, Europe, and Asia-Pacific.

Head OfficeMira Road East, Mumbai, India
Plant LocationRajkot Industrial Zone, Gujarat
System CertificationISO 9001:2015 Quality Management
EU CompliancePED 2014/68/EU (TÜV Rheinland)
Testing LabIn-House PMI, Tensile, Impact, Hardness
Inspection ReleaseEN 10204 Type 3.1 & Type 3.2
100% In-House PMI Verification Every single C276 fastener undergoes handheld XRF spectrometry before packaging to verify exact Cr, Mo, W, and Ni elemental compliance.
TÜV Rheinland PED Approved Certified under Pressure Equipment Directive 2014/68/EU Annex I, Section 4.3 for critical European pressure boundary equipment.
Dual EN 10204 3.1 & 3.2 Supply Mill certificates accompanied by standard batch reports or fully witnessed by DNV, Bureau Veritas, Lloyd's Register, or SGS.
Fast-Track Shutdown Services Dedicated production cells capable of 48-hour turnarounds on urgent replacement C276 studs and nuts during unscheduled plant shutdowns.
RFQ Guide

How to Specify Hastelloy C276 Fasteners for Fast Quotation

To avoid metallurgical mismatch, lengthy engineering clarifications, and delivery delays, verify your procurement inquiry against our engineering specification parameters:

Alloy Specification
Hastelloy C276 / UNS N10276 / DIN 2.4819 / ASTM B574
Fastener Standard
ASME B18.2.1 (Bolts), ASME B18.31.2 (Studs), ASME B18.2.2 (Nuts), DIN 931/934
Size & Thread Class
Nominal diameter, thread pitch (UNC, 8UN, Metric Coarse/Fine), Class 2A/2B fit
Heat Treatment
Solution Annealed (standard / NACE sour service) or Strain-Hardened (high strength)
Surface Finish
Pickled/Passivated, PTFE Fluoropolymer, Xylan 1070, MoS2, or Silver Plated
Quality Documentation
EN 10204 3.1, EN 10204 3.2 (Agency witnessed), NACE MR0175, ASTM G28 IGC
Quantity & Schedule
Exact piece counts (plus installation spares) and required site delivery date

Ready to Consult with Our Metallurgical Engineers?

Whether you require standard ANSI flange studs, large-diameter custom reactor bolts, or technical advice on avoiding thread galling in high-pressure acid piping, our technical sales engineers are available around the clock.

Get in touch now to receive instant stock status, competitive manufacturer pricing, and comprehensive technical submittals.

Contact Us