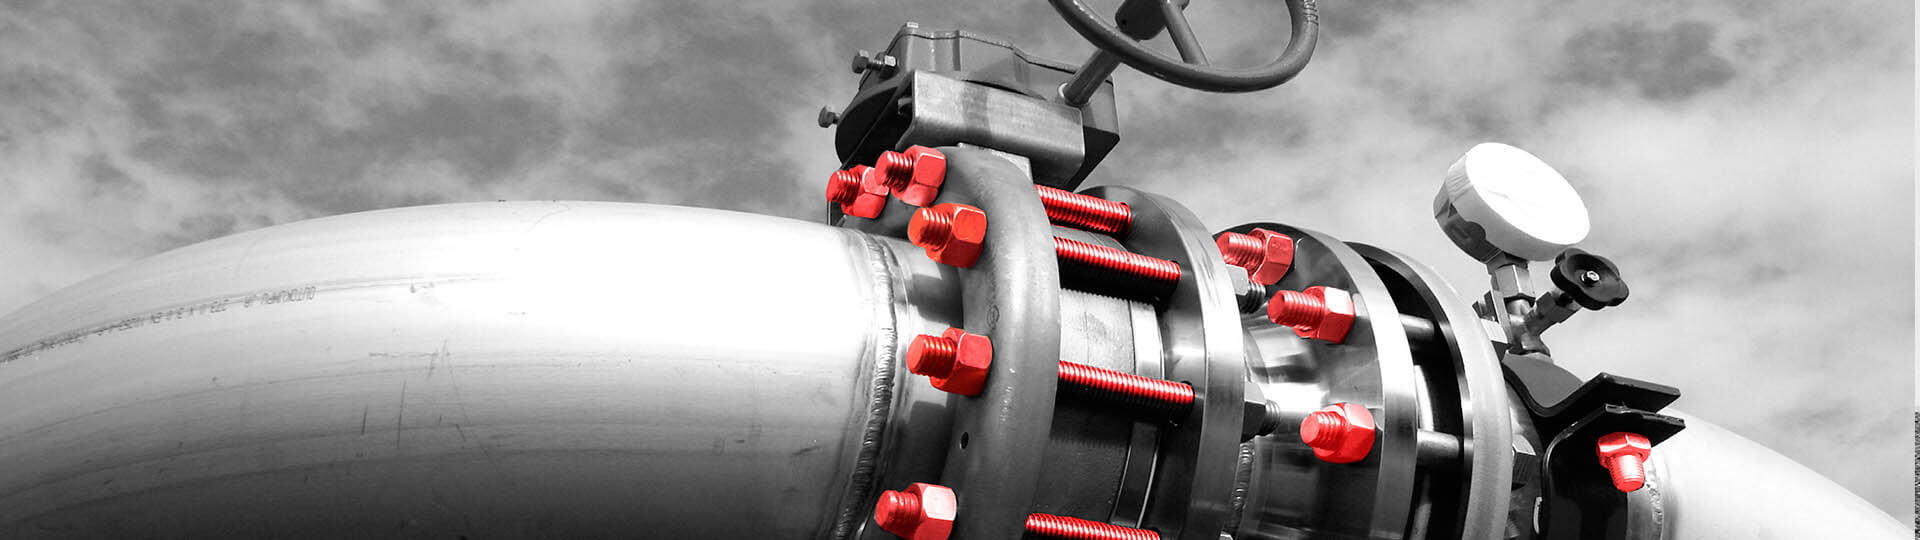
High performance Waspaloy and superalloy stud bolts with heavy hex nuts for turbine casings and critical flange assemblies
Precision-machined high-temperature superalloy washers and bolting components
ISO 9001:2015Rigorous aerospace-grade QA system
PED 2014/68/EUTUV Rheinland approved pressure parts
EN 10204 3.1 / 3.2100% VIM-VAR heat traceability
Since 2010Exporting to 45+ global markets

Waspaloy Fasteners: The Complete Engineering & Global Procurement Guide

When continuous operating environments exceed 1200°F (650°C), conventional austenitic stainless steels and even standard precipitation-hardened superalloys face rapid microstructural degradation. Waspaloy Fasteners (UNS N07001 / W.Nr. 2.4654) provide the ultimate metallurgical answer for rotating turbine assemblies, aerospace propulsion, rocket motor casings, and hyper-critical energy installations.

Manufactured by TorqBolt Inc. across our state-of-the-art facilities in Rajkot and Mumbai, India, our Waspaloy bolting line is engineered from premium vacuum-melted (VIM-VAR) feedstock. We supply high-integrity hex head bolts, double-end stud bolts, socket cap screws, and matched heavy hex nuts compliant with AMS 5708, AMS 5709, and ASTM B637 specifications. By maintaining precise multi-stage solution and stabilization heat-treatment regimes, TorqBolt guarantees unyielding creep-rupture life and shear strength up to 1600°F (870°C).

Product Engineering & Selection

Recommended Waspaloy Fastener Configurations

Every industrial application subjects fasteners to distinct tensile, rotational, and thermodynamic shear stresses. TorqBolt hot forges and CNC machines Waspaloy fasteners to tight aerospace tolerances (Class 3A/3B UN threads and ISO 4h/6g metric fits), eliminating stress concentrations at thread run-outs and head fillets.

Waspaloy hex head bolt manufactured to AMS 5708 and ASTM B637 standards

Waspaloy Hex Head Bolts

Optimized for structural gas turbine casing flanges, exhaust manifolds, and high-pressure compressor stages requiring high yield strength.

Standards: AMS 5708, ASME B18.2.1, DIN 931, ISO 4014
Inquire About Hex Bolts
Waspaloy fully threaded stud bolt for extreme temperature turbine and valve flanges

Waspaloy Stud Bolts

Full-thread, double-end, and tap-end engineered studs with rolled threads to prevent stress crack corrosion and relaxation under cyclic thermal expansion.

Standards: ASTM B637, ASME B16.5, DIN 976, UNC / 8UN
Inquire About Studs
Waspaloy heavy hex nut with silver plating to eliminate galling in extreme heat

Waspaloy Hex & Heavy Nuts

Precision-tapped hex and heavy hex nuts paired with silver plating (AMS 2410) to eliminate high-temperature galling, seizure, and mating thread friction.

Standards: ASME B18.2.2, AMS 5708, ISO 4032, DIN 934
Inquire About Nuts
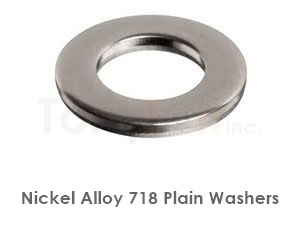
High temperature Waspaloy flat and Belleville spring washers

Waspaloy Precision Washers

Flat, hardened, and conical spring Belleville washers maintaining pre-load tension under severe thermal expansion and vibration.

Standards: ASME B18.21.1, DIN 125, DIN 6796, Custom Drawing
Inquire About Washers
Custom Geometries: Socket Head Cap Screws Continuous Threaded Rod 12-Point Flange Bolts D-Head Aircraft Bolts Countersunk Screws Tie Rods & Turnbuckles Waspaloy Product Center
Metallurgical Authority

Waspaloy vs. Competing Superalloys: Chemical & Creep Analysis

Understanding why Waspaloy outclasses alternative nickel-chromium alloys requires examining its metallurgical matrix. While Inconel 718 relies on body-centered tetragonal γ″ (Ni3Nb) precipitates that coarsen rapidly above 1200°F (650°C) and transform into brittle delta phase, Waspaloy utilizes a high-volume fraction of coherent face-centered cubic γ′ [Ni3(Al, Ti)] precipitates stabilized by 12–15% cobalt and 3.5–5.0% molybdenum. This enables Waspaloy to maintain outstanding yield strength, thermal fatigue limits, and oxidation resistance up to 1600°F (870°C).

Chemical Composition Breakdown: Waspaloy (UNS N07001 / 2.4654) vs Alternative High-Temp Fastener Alloys
Element Waspaloy (UNS N07001) Inconel 718 (UNS N07718) Inconel 625 (UNS N06625) A-286 (UNS S66286)
Nickel (Ni)Balance (55.0 – 61.0%)50.0 – 55.0%58.0% min24.0 – 27.0%
Chromium (Cr)18.00 – 21.00%17.00 – 21.00%20.00 – 23.00%13.50 – 16.00%
Cobalt (Co)12.00 – 15.00%1.00% max1.00% max—
Molybdenum (Mo)3.50 – 5.00%2.80 – 3.30%8.00 – 10.00%1.00 – 1.50%
Titanium (Ti)2.75 – 3.25%0.65 – 1.15%0.40% max1.90 – 2.35%
Aluminum (Al)1.20 – 1.60%0.20 – 0.80%0.40% max0.35% max
Niobium (Nb/Cb)—4.75 – 5.50%3.15 – 4.15%—
Iron (Fe)2.00% maxBalance (approx. 17%)5.00% maxBalance (approx. 55%)
Carbon (C) / Boron (B)0.02 – 0.10% C / 0.003 – 0.010% B0.08% C max / 0.006% B0.10% C max0.08% C max / 0.003 – 0.010% B
Max Operating Temp1600°F (870°C)1200°F (650°C)1100°F (593°C)1000°F (538°C)

Composition complies with AMS 5708, AMS 5544, and ASTM B637. Chemical analysis verified per batch via Optical Emission Spectrometry (OES) and Inductively Coupled Plasma (ICP) testing.

Manufacturing Integrity

Engineering Precision: The TorqBolt Heat Treatment & Thread Rolling Process

Unlike standard stainless hardware, Waspaloy cannot achieve its mechanical parameters through simple cold working. Achieving peak tensile strength (175–185 ksi) combined with notch rupture ductility requires an exacting multi-phase precipitation cycle executed in computer-controlled atmosphere furnaces.

The 4-Stage Heat Treatment Cycle

Our Rajkot manufacturing facility adheres strictly to the AMS 5708 heat treatment regimen to stabilize γ′ precipitates and distribute grain boundary carbides:

1. Solution Anneal 1975°F ± 25°F (1080°C) for 4 hours; rapid water/oil quench to hold matrix elements in solid solution.
2. Stabilization Treatment 1550°F ± 15°F (845°C) for 4 hours; air cool. Precipitates M23C6 carbides at grain boundaries to block grain boundary sliding.
3. Primary Age Hardening 1400°F ± 15°F (760°C) for 16 hours; air cool. Generates dense dispersion of sub-micron γ′ [Ni3(Ti, Al)] strengthening phases.
4. Secondary Aging Step 1200°F ± 15°F (650°C) for 16 hours; air cool. Enhances low-cycle fatigue limits and relives localized micro-strains.

Thread Rolling vs Cut Threads

Thread geometry is the primary focal point of fatigue failure under cyclic thermal loading. TorqBolt enforces strict thread forming parameters:

  • Continuous grain flow contours conforming to root radii
  • Up to 300% improvement in dynamic fatigue fatigue resistance
  • Zero micro-tear root defects verified via optical comparators
  • UNJ aerospace thread profile (ASME B1.15) with generous root radiusing
  • 100% thread pitch and flank diameter validation via tri-roll gauges
  • Roll threading performed prior to final age hardening for residual compression
Operating Domains

Mission-Critical Environments for Waspaloy Bolting

TorqBolt fasteners operate where component failure entails catastrophic system loss. Our Waspaloy bolting line is deployed across international aerospace tiers, turbine OEMs, and heavy energy infrastructures.

Aviation & Jet Engines

Compressor and turbine disc bolting, nozzle guide vane retainers, and thrust reverser hardware exposed to intense thermal gradients.

Land-Based Gas Turbines

Combustion transition ducts, hot gas path outer casings, and blade locking fasteners requiring unyielding resistance to 1400°F creep.

Space & Rocket Propulsion

Liquid rocket engine injector heads, turbopump housings, and combustion chamber tie-bolts subjected to cryogenic-to-pyrotechnic shock.

Nuclear & High-Pressure Steam

Supercritical boiler suspension hardware, core structural fasteners, and high-temperature steam turbine control valves.

Procurement Checklist

Waspaloy RFQ Formulation Guide for Procurement Engineers

Due to the cost of raw nickel, cobalt, and molybdenum, imprecise inquiries result in costly revision cycles. To obtain immediate metallurgical feasibility and fixed pricing, ensure your RFQ incorporates the following mandatory criteria:

Material Grade & Melt
Waspaloy / UNS N07001 / Werkstoff 2.4654 with VIM-VAR melt specification
Governing Standard
AMS 5708, AMS 5709, ASTM B637, ASME SB637, or OEM drawing specification
Heat Treat Condition
Solution Annealed, Double Aged, or Fully Hardened (AMS 5708 4-stage cycle)
Thread Profile
UNJ (Class 3A/3B), UNC, UNF, 8UN, or ISO Metric with controlled root radii
Plating & Anti-Galling
Silver Plating per AMS 2410 / AMS 2411, Molybdenum Disulfide, or Degreased Plain
Destructive Testing
ASTM E139 Creep Rupture at 1350°F (732°C) or 1500°F (815°C), Elevated Tensile
Certification Level
EN 10204 3.1 with chemical/mechanical results; EN 10204 3.2 Third-Party Witnessed

TorqBolt Manufacturing Advantage

Since 2010, TorqBolt Inc. has been the go-to exotic fastener manufacturer for international engineering firms. With dual facilities in Mumbai and Rajkot, we bridge the gap between high-volume forging economy and micro-tolerance aerospace precision.

Quality CertificationISO 9001:2015
Pressure DirectivePED 2014/68/EU (TUV)
In-House LabsPMI, Spectro, Hardness & UTS
Export FootprintNorth America, Europe, Middle East
Technical Knowledge Hub

Frequently Asked Questions on Waspaloy Fasteners

Detailed technical answers addressing the most critical questions posed by piping designers, mechanical integrity teams, and procurement analysts.

Why choose Waspaloy fasteners over Inconel 718 for critical applications?
While Inconel 718 is widely used up to 1200°F (650°C), its strengthening γ″ (gamma double prime) phase rapidly over-ages, losing coherency and precipitating into the non-strengthening needle-like delta (δ) phase at prolonged temperatures above 1200°F. This leads to dramatic loss in yield strength and catastrophic creep failure. Waspaloy (UNS N07001), on the other hand, is hardened via γ′ [gamma prime - Ni3(Al,Ti)] precipitates that remain stable up to 1600°F (870°C), reinforced by 12–15% cobalt that lowers stacking-fault energy. This metallurgical composition gives Waspaloy superior stress-rupture life, thermal shock resistance, and oxidation resistance in gas turbine combustors and jet engines.
What heat treatment profile is mandated for aerospace-grade AMS 5708 Waspaloy fasteners?
Aerospace Waspaloy fasteners manufactured under AMS 5708 undergo an exhaustive four-step heat treatment process:
  1. Solution Heat Treatment: 1975°F ± 25°F (1080°C) for 4 hours, followed by rapid air cooling or oil quench to dissolve intermetallic phases into the austenitic nickel matrix.
  2. Stabilization Annealing: 1550°F ± 15°F (845°C) for 4 hours, air cooling. This crucial stage precipitates chromium carbides along grain boundaries to inhibit grain-boundary sliding under high stress.
  3. First Precipitation Aging: 1400°F ± 15°F (760°C) for 16 hours, air cooling. Forms primary uniform γ′ hardening precipitates.
  4. Second Precipitation Aging: 1200°F ± 15°F (650°C) for 16 hours, air cooling. Fine-tunes precipitate size distribution and increases yield strength above 115 ksi at 1400°F.
How does TorqBolt mitigate high work-hardening rates and micro-cracking when machining Waspaloy?
Waspaloy is notoriously difficult to machine due to abrasive titanium carbides, low thermal conductivity (which traps intense heat at the tool-workpiece interface), and an extreme strain-hardening exponent. TorqBolt overcomes this using high-rigidity CNC machining platforms equipped with high-pressure through-spindle coolant systems operating at 70 bar to immediately dissipate heat. We utilize specialized positive-rake PVD TiAlN-coated carbide or whisker-reinforced ceramic inserts, maintaining heavy, continuous tool feeds to stay underneath the work-hardened surface layer. Crucially, thread rolling is utilized rather than thread cutting, ensuring dense, compressive residual stresses in the thread roots that safeguard against dynamic fatigue cracking.
What non-destructive and destructive QA certifications accompany TorqBolt Waspaloy fasteners?
TorqBolt supplies every Waspaloy fastener shipment with a comprehensive EN 10204 Type 3.1 inspection certificate (with Type 3.2 third-party witnessed inspection available through TUV, DNV, Lloyd's, or Bureau Veritas). Testing documentation covers:
  • Full chemical heat analysis traceable to the original VIM-VAR melt.
  • Room temperature tensile, yield, and elongation testing per ASTM E8.
  • High-temperature tensile testing at 1200°F / 1400°F per ASTM E21.
  • Stress-rupture testing per ASTM E139 (guaranteeing minimum rupture life under specified load at 1350°F / 1500°F).
  • Fluorescent Penetrant Inspection (FPI) per ASTM E1417 / AMS 2644 to confirm zero linear indications or micro-cracks on heads and rolled threads.
  • 100% Positive Material Identification (PMI) via XRF/OES analyzers.
What surface coatings and lubrication treatments are recommended for Waspaloy bolting?
Standard PTFE and zinc-based coatings decompose rapidly above 500°F (260°C) and cannot be used with Waspaloy. At continuous operating ranges between 1000°F and 1600°F, high-temperature thread galling and diffusion bonding (welding of mating threads) present critical challenges. TorqBolt applies precision electrolytic Silver Plating per AMS 2410 or AMS 2411 over an active nickel strike on mating nuts or stud threads. Silver acts as a solid lubricious barrier up to 1400°F, ensuring predictable make-up torque and non-destructive disassembly during gas turbine overhaul cycles. Alternatively, proprietary ceramic-metallic slurries or baked MoS2 dry film lubricants are supplied for intermediate temperature ranges.
Contact Us