
Supplying global tier-1 infrastructure, offshore energy platforms, subsea manifolds, and hyper-critical chemical plants with rigorously vetted bolting assemblies.
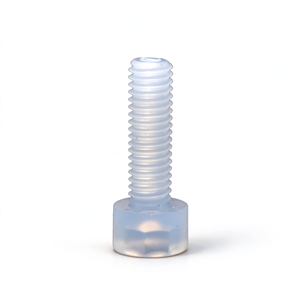
Superior dielectric insulation and absolute chemical inertness designed for acid wet-benches and severe chemical immersion.
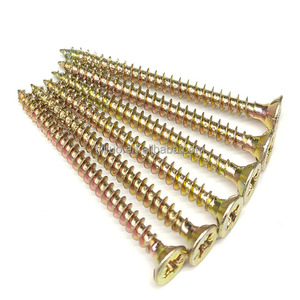
Serrated thread geometry engineered for anti-splitting structural assemblies with superior torque-shear retention.
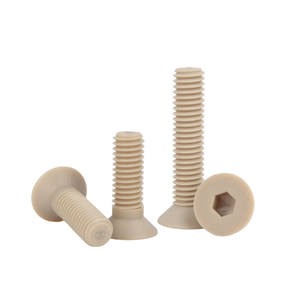
Countersunk flat-head designs offering ultra-low outgassing and high mechanical rigidity for wafer fabrication chambers.
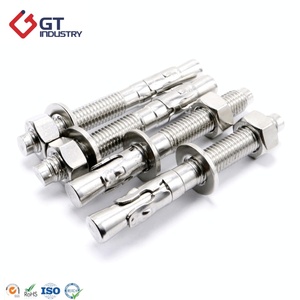
Heavy-duty expansion systems engineered for high shear and pull-out resistance in splash zones and coastal installations.
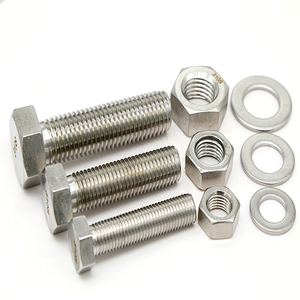
Microstructure-controlled duplex bolting with yield strength over 550 MPa, optimized for subsea risers and sour service.
Unrivalled resistance to fast-flowing seawater, de-aerated hydrofluoric acid, and stress cracking under API 6A parameters.
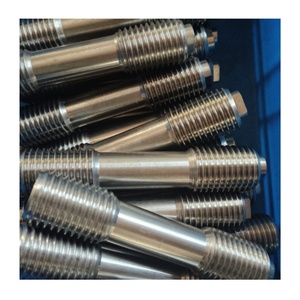
Full-thread continuous studding matched to A194 grade nuts, certified to withstand elevated cyclical thermal fatigue.
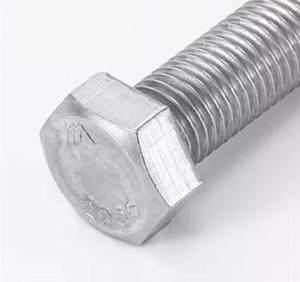
Ultimate resistance to pitting, stress-corrosion cracking, and oxidizing environments across DIN 933, DIN 934, and ASME B18.2.1.
In high-tensile and mission-critical bolting, mechanical failure is rarely an isolated metallurgical defect; it is typically an engineering mismatch where hydrogen embrittlement, stress corrosion cracking (SCC), or localized galvanic degradation compromises structural pre-load. As an established high-tensile fastener factory and worldwide exporter, our operational standards surpass conventional commercial manufacturing by applying stringent continuous heat-treat validation and hot-forged microstructural alignment.
| Material Class | UNS / Spec | Tensile Strength (MPa) | Yield Strength (0.2%, MPa) | Operating Limit (°C) | Primary Industrial Sector |
|---|---|---|---|---|---|
| Inconel 718 | UNS N07718 / API 6A CRA | ≥ 1240 | ≥ 1034 | -250 to +650 | Subsea Trees, Gas Turbines |
| Super Duplex 2507 | UNS S32750 / EN 1.4410 | ≥ 750 | ≥ 550 | -50 to +300 | Offshore Desalination, Swivel Joints |
| Hastelloy C-276 | UNS N10276 / ASTM B574 | ≥ 690 | ≥ 283 | -196 to +400 | FGD Scrubbers, Sulfuric Processing |
| High-Tensile A453 660 | UNS S66286 / Grade A/B/C/D | ≥ 895 | ≥ 585 | -29 to +700 | High-Pressure Steam Flanges |
| Titanium Grade 5 | UNS R56400 / Ti-6Al-4V | ≥ 895 | ≥ 828 | -250 to +400 | Aerospace, Subsea Autonomous Vehicles |
Precision thread rolling—executed exclusively after solution annealing and precipitation heat treatment—maintains uninterrupted compressive grain flows around the thread root, substantially boosting the dynamic fatigue threshold. Where sour hydrocarbon service governs design, our QA ensures that final hardness strictly adheres to NACE MR0175 / ISO 15156 thresholds (HRC ≤ 35 for 718 CRA, HRC ≤ 28 for Duplex), completely preventing sulfide stress corrosion cracking under deep-well conditions.
Procurement directors and supply chain managers are realigning their sourcing strategies away from fragmented commodity brokers toward vertically integrated manufacturers capable of proving chemical ancestry. The evolving landscape presents clear structural shifts:
Global operators now mandate independent third-party inspection (Lloyd's Register, DNV, ABS, TÜV) witnessing raw billet melt, destructive tensile testing, and Charpy V-notch impacts down to -46°C or -196°C.
Traditional zinc electroplating is being displaced by Xylan 1070, PTFE, and ceramic-infused fluoropolymer coatings that guarantee over 3,000 to 5,000 hours of ASTM B117 salt spray endurance without galling.
Rather than standard sizes only, major EPCs require integrated forging facilities capable of rapid-prototyping custom non-standard shank diameters, step-studs, and heavy-duty socket cap screws via 5-axis CNC machining.
As operating parameters push into deeper subsea environments, hydrogen fuel transmission, and supercritical CO2 sequestration, fastener durability is advancing across several fronts:
Additive-Forging Hybrids: Integration of laser-clad wear surfaces with hot-forged alloy cores provides customized wear and corrosion profiles while retaining primary high-tensile core properties.
Digital Ultrasonic Tension Monitoring: Next-generation offshore installations are implementing bolts embedded with calibrated piezoelectric sensor transducers, enabling technicians to read clamp load directly in real time, bypassing inaccurate torque approximations.
Sustainable Eco-Passivation & Chrome-Free Passivation: Environmental regulations (REACH/RoHS) are accelerating the phase-out of hexavalent chromium coatings in favor of high-adhesion organo-mineral systems with non-electrolytic dip-spin application routes that completely eliminate the risk of hydrogen absorption during plating.
Fully certified under ISO 9001:2015 and PED 2014/68/EU by TÜV Rheinland, satisfying mandatory European pressure vessel compliance for power and chemical equipment.
Our Rajkot production center features comprehensive in-house mechanical labs: Positive Material Identification (PMI via XRF/OES), Charpy impact, tensile, micro-hardness, and intergranular corrosion testing.
Exporting to over 45 countries with tailored marine packing, comprehensive documentation sets, and express customs-cleared dispatch to North America, Europe, the Middle East, and APAC.
Connect with our technical engineering desk. Get our comprehensive alloy selection handbook, coating compatibility matrices, and verified pricing schedules for your next planned project or urgent turnaround.
Get Catalog