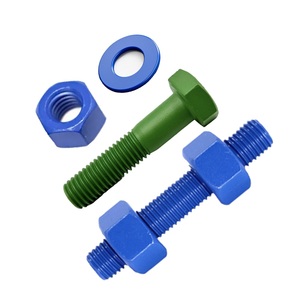
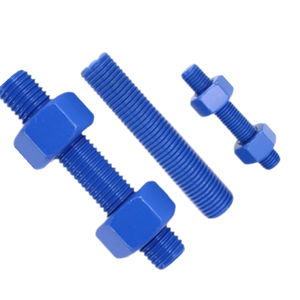
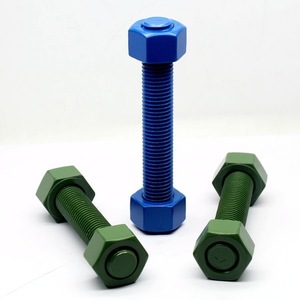
China Top Xylan Coated Bolts Manufacturers & Suppliers

Specialized Engineering Whitepaper & Global Sourcing Guide for High-Integrity Fluoropolymer (PTFE / Xylan®) Stud Bolts, Heavy Hex Bolts, and Subsea Bolting Assemblies

4,000+ Hrs
ASTM B117 Salt Spray Durability
ISO & PED
TÜV Rheinland Certified QA
0.05 - 0.08
Stable Kinetic Friction (μ)
50+ Countries
Global Energy & Marine Deployments
Product Catalog

Engineered Xylan® & PTFE Coated Fastener Solutions

Explore our precision-manufactured fluoropolymer-bonded stud bolts, heavy hex bolts, and specialized industrial hardware tailored for extreme marine, chemical, and offshore environments.
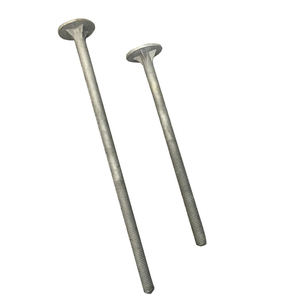
A307 Round Head Nip Bolts Crane Mat Rod Hot-Dip Galvanized Timber Bolt

A307 Round Head Nip Bolts Crane Mat Rod Hot-Dip Galvanized Timber Bolt

Substrate: ASTM A307 Grade A/B Carbon Steel
Surface Finish: HDG / Dual PTFE Seal Option
Application: Heavy Foundation & Marine Crane Mats
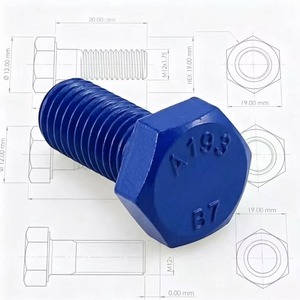
PTFE Xylan Coated Anti Corrosion ASTM A193 B7 Alloy Steel Heavy Hex Bolts

PTFE Xylan Coated Anti Corrosion ASTM A193 B7 Alloy Steel Heavy Hex Bolts for Oil Gas

Substrate: AISI 4140 Quenched & Tempered
Coating: Genuine Xylan® 1424 / 1070 Blue
Operating Temp: -40°C to +205°C Continuous
ASTM A194 2H Heavy Hex Bolts PTFE Bolts and Nuts A193 B7 B8 Xylan 1424

Astm A194 2H Heavy Hex Bolts PTFE Bolts and Nuts A193 B7, B8 Xylan 1424, Blue Stud Bolts Nuts ISO 7089 Wahsers F 3125 A325

Configuration: Bolt, 2H Heavy Nut & Washer Set
Standard: ASME B18.2.1, B18.2.2, ASTM F3125
Anti-Galling: Dry Film Lubricant Layer
Industrial Parts Manufacturer M8 M28 PTFE Xylan 1424 1014 1070 Fluoropolymer Coated Hex Bolt

Industrial Parts Manufacturer M8 M28 PTFE Xylan 1424/xylan 1014 1070 Fluoropolymer Coated Hex Bolt

Size Range: Metric M8 to M28 / Imperial 3/8" to 1-1/8"
Resin Chemistry: Fluoroelastomer Blend (Xylan 1014)
Corrosion Resistance: 3,000+ Hrs ASTM B117
Xylan Blue Coated Bolts and Nuts Custom Surface Treatments

Xylan Blue Coated Bolts & Nuts | Custom Surface Treatments | Anti-Corrosion & Low Friction

Pre-treatment: Zinc / Manganese Phosphatizing
Thickness: 25 ± 5 μm (Controlled Pitch Allowance)
Color Codes: Standard Blue, Red, Yellow, Forest Green
PTFE Fluorocarbon Xylan Coating ASME B18.2.1 ASTM B7 B8 Stud Bolt

PTFE Fluorocarbon Xylan Coating ASME B18.2.1 ASTM B7/B8 Astm A193 Thread Rod Stud Bolt B7 B16

Standards: ASME B16.5 Piping, ASTM A193 B16
Basecoat Options: Thermal Diffusion or Zinc-Nickel
High Temp Duty: Resistant to Thermal Creep
PTFE Xylan Fluoropolymer Coated Stainless Steel Stud Bolt ASTM A193 Gr B7

PTFE Xylan Fluoropolymer Coated Stainless Steel Stud Bolt Astm A193 Gr B7

Substrates: Duplex 2205 / SS316 / Alloy B7
Anti-Galling: Eliminates Stainless-on-Stainless Seizure
Traceability: EN 10204 3.1 Heat Number Stamping
ASTM 4140 B7 B8 A193 A194 A194m PTFE Xylan Stud Bolts

ASTM 4140 B7 B8 A193 A194 A194m A194m PTFE Xylan Stud Bolts

Threading: CNC Precision UNC / 8UN Class 2A/2B
Coating Spec: Whitford Approved Application Standard
NACE MR0175: Hardness Controlled ≤ 22 HRC Sour Duty
Inquire Now
Technical Engineering

The Science of Fluoropolymer Surface Barrier Engineering

In harsh petrochemical processing, subsea exploration, and high-salinity coastal infrastructure, standard galvanic zinc or cadmium plated fasteners experience rapid interfacial depletion. As China's premier manufacturer and supplier of engineered bolting, we formulate multi-layer fluoropolymer dry film barrier coatings based on authentic Whitford Xylan® resin technology (Xylan 1070, 1014, 1424) to provide extreme mechanical durability and chemical isolation.

Xylan® is a composite coating engineered from high-molecular-weight polytetrafluoroethylene (PTFE) and other fluoro-monomers bonded within heat-cured, high-tensile resins such as polyamide-imide (PAI) and polyphenylene sulfide (PPS). This matrix yields a non-porous, hydrophobic barrier that stops corrosive media (chlorides, hydrogen sulfide, sulfuric acid, and ambient moisture) from contacting the load-bearing alloy substrate.

  • Galvanic Isolation & Dissimilar Metal Compatibility: Xylan acts as a dielectric insulator, preventing electrochemical cell creation between stainless steel, duplex, or nickel alloys and carbon steel flange faces.
  • Controlled Coefficient of Friction: Uniform kinetic friction coefficient (μ = 0.05 to 0.08) eliminates thread chatter, galling, and seizure, translating applied torque directly into precise bolt pre-load clamping force.
  • Zero Hydrogen Embrittlement Risk: When paired with mechanical pre-treatments or thermal diffusion basecoats, our application process circumvents the cathodic acid-pickling cycles typical of electroplating.

Cross-Section Coating Architecture

Our precision coating envelope adheres to strict thickness tolerances (20–35 μm) to guarantee class 2A/2B fit without compromising thread pitch geometry:

Layer 3: Topcoat (15-20 μm) Xylan® 1070 / 1424 fluoropolymer matrix providing low friction, color identification, and chemical resistance.
Layer 2: Primer / Basecoat (5-10 μm) Thermosetting phenolic/epoxy resin primer engineered for molecular inter-coat crosslinking and substrate bonding.
Layer 1: Pre-treatment (2-5 μm) Manganese or Zinc Phosphate (MIL-DTL-16232) or micro-crystalline thermal diffusion over Sa 2.5 white-metal blasted substrate.
Technical Matrix

Engineering Comparison: Fastener Surface Treatments

A comprehensive metallurgical benchmark evaluating anti-corrosion barrier performance, torque predictability, and operating envelope across standard bolting finishes.

Coating Specification Salt Spray (ASTM B117) Service Temp (°C) Friction Coeff (μ) Galling Resistance Sour Service (H2S) Primary Industrial Sector
Xylan® 1070 (PTFE / Resin) 3,000 – 4,200 Hrs -195 to +260 °C 0.06 – 0.10 Superior Compliant (NACE) Offshore Platforms, Subsea Wellheads
Xylan® 1424 (Waterborne) 1,500 – 3,000 Hrs -40 to +180 °C 0.08 – 0.12 Superior Compliant Chemical Processing, Coastal Flanges
Xylan® 1014 (High-Luster) 2,500 – 3,500 Hrs -195 to +260 °C 0.05 – 0.08 Maximum Compliant Valve Actuators, Deep-water Drilling
Hot-Dip Galvanizing (ASTM A153) 500 – 1,000 Hrs Up to +200 °C 0.18 – 0.25 Poor / Seizure Risk Conditional Structural Steel, Bridges, Transmission
Zinc-Nickel Electroplate 1,000 – 1,500 Hrs -50 to +150 °C 0.12 – 0.16 Moderate Subject to Cracking Automotive, Light Marine Deck
Cadmium + Chromate (AMS-QQ-P-416) 500 – 1,000 Hrs Up to +230 °C 0.12 – 0.14 Good Toxic / Restricted Legacy Aerospace (Phasing Out)

*Note: Salt spray hours depend directly on the pre-treatment basecoat (e.g., zinc phosphating vs. zinc-nickel undercoat) and total dry film thickness (DFT).

Manufacturing QA

Precision Multi-Stage Application Process

Our standardized 7-step fluoropolymer deposition sequence is executed in climate-controlled clean rooms, ensuring micro-level adhesion, consistent thread tolerance, and total heat traceability.

1
Abrasive Blasting
Sa 2.5 white metal profile (25-45 μm) with chilled iron grit for mechanical tooth lock.
2
Chemical Pre-treat
Manganese or Zinc Phosphating (MIL-DTL-16232) providing an anti-corrosion chemical base.
3
Adhesion Primer
Automated robotic spray of liquid resin primer to eliminate inter-laminar delamination.
4
Xylan® Spraying
Precision multi-axis electrostatic or dip-spin spray maintaining 25±5 μm uniform coating.
5
Thermal Sintering
Computer-controlled convection curing at 200°C–400°C for complete fluoropolymer crosslinking.
6
QA Laboratory
ASTM D3359 cross-hatch, eddy-current DFT inspection, and NACE SP0188 holiday testing.
7
MTR & Packaging
Laser marking, EN 10204 3.1 certification generation, and export seaworthy crating.
Why Choose Us

Enterprise Strengths & Factory Capabilities

Combining advanced forging, CNC bar machining, and in-house laboratory testing under rigorous ISO and PED accreditations to serve critical projects worldwide.

TÜV Certified Quality System

Fully certified under ISO 9001:2015 and PED 2014/68/EU by TÜV Rheinland. We ensure full adherence to European Pressure Equipment Directives for high-pressure boilers, heat exchangers, and subsea pipelines.

Certified Compliance

Exotic Metallurgy & Alloy Range

Beyond standard ASTM A193 B7/B16 and A194 2H, our production facilities process Inconel 625/718, Hastelloy C276, Monel 400, Duplex 2205, Super Duplex 2507, and Titanium Grade 5 with proprietary Xylan adhesion formulations.

High-Alloy Ready

EN 10204 3.1 / 3.2 Traceability

Every lot comes standard with an EN 10204 3.1 mill test certificate linking the physical fastener to the original melt heat number. Independent third-party inspection (3.2) witnessed by Lloyd's Register, DNV, or SGS is readily facilitated.

100% Heat Batch Traceable

Forging & Precision CNC Machining

Our workshops house multi-station cold headers, 1,000-ton hot forging presses, and 5-axis CNC machining centers. This allows us to produce both high-volume standard fasteners and custom bespoke drawings from M6 to M120.

Custom Geometries

NACE MR0175 / ISO 15156 Sour Duty

For severe upstream environments containing wet H2S, we implement strict heat treatment schedules and hardness inspection routines, guaranteeing maximum hardness readings ≤ 22 HRC to prevent sulfide stress cracking (SSC).

Sour Service Certified

Turnkey Global Export Logistics

Supplying offshore EPC projects, drilling shipyards, and LNG terminals across North America, the Middle East, Southeast Asia, and Europe. Dedicated export packaging protects coated thread flanks during intercontinental ocean transit.

Global Door-to-Site
Industry Insights

Future Procurement & Technological Trends (2025–2030)

How changing environmental regulations, deepwater offshore developments, and digital asset management are transforming global fastener procurement strategies.

PFAS-Safe & Low-VOC Formulations

With stringent REACH and EPA restrictions emerging around poly-fluoroalkyl substances, chemical research is advancing waterborne formulations such as Xylan® 1424 and ceramic-infused bio-neutral resins that maintain 3,000+ salt-spray hours without hazardous emissions.

Regulatory Evolution →

Deepwater & Subsea Extreme Service

High-pressure, high-temperature (HPHT) subsea reservoirs operating beyond 15,000 psi require double-barrier coatings: combining micro-crystalline thermal diffusion zinc basecoats with engineered PTFE topcoats to completely resist cathodic delamination under hydrostatic heads.

Subsea Resiliency →

Digital Traceability & Smart Fasteners

The procurement landscape is migrating toward 2D data-matrix laser engraving on bolt heads. In-situ technicians scan stud bolts via mobile tools to instantly retrieve mill chemical records, batch torquing profiles, and previous inspection timestamps.

Industry 4.0 Bolting →

TCO & Zero Hot-Bolting Maintenance

Procurement executives prioritize Total Cost of Ownership (TCO) over initial unit cost. Coated fasteners ensure breakout torque matches tightening torque, eliminating torch cutting, hydraulic nut splitting, and unscheduled refinery turnaround delays.

TCO Optimization →
Knowledge Base

Frequently Asked Technical & Sourcing Questions

Answers to common engineering inquiries regarding thread allowances, coating chemistries, tightening factors, and certification compliance.

What is the key difference between Xylan® 1070 and Xylan® 1424 coatings?
Xylan® 1070 is a solvent-borne fluoropolymer coating formulated with high-tensile organic binders and PTFE lubricants, providing optimal operating ranges (-195°C to +260°C) and superior salt spray resistance (up to 4,200 hours). Xylan® 1424 is an environmentally friendly, waterborne, low-VOC alternative offering comparable low friction (μ = 0.08–0.12) with a slightly lower operating ceiling (+180°C). Both provide outstanding anti-galling and corrosion resistance for oilfield flange bolting.
How do you accommodate coating thickness on bolt thread dimensions?
Applying 20–35 μm (0.0008"–0.0014") of fluoropolymer coating adds four times the thickness to the pitch diameter of 60° threads. To prevent thread interference during assembly, our CNC threading and cold-rolling lines utilize Class 2A thread pitch allowances, or custom undercut dimensions (e.g., 6g/6e for metric) prior to coating, ensuring smooth engagement with standard 2H/Grade 8 heavy hex nuts without nut tapping alterations.
Can Xylan coated bolts eliminate thread galling in stainless steel and duplex alloys?
Yes. Stainless steel (ASTM A193 B8/B8M) and duplex/super duplex alloys (2205 / 2507) tend to gall and cold-weld under preload torque due to localized friction tearing their passive chromium oxide film. A factory-applied Xylan® coating serves as a dry-film lubricating barrier, completely preventing metal-to-metal contact and micro-welding during torque cycling.
What documentation and test certificates are supplied with every order?
All shipments include an EN 10204 Type 3.1 Inspection Certificate that documents chemical composition, heat numbers, tensile and yield strength, elongation, Charpy V-notch impact values (where mandated), and Rockwell hardness. For coated bolts, we append Dry Film Thickness (DFT) verification, cross-hatch adhesion reports (ASTM D3359 Method B), and optional third-party (EN 10204 3.2) witnessed inspection certificates from ABS, DNV, or Lloyd's Register.
How does fluoropolymer coating prevent hydrogen embrittlement?
Hydrogen embrittlement commonly occurs in high-strength steels (like ASTM A193 B7 and A490) during aggressive electroplating acid pickling. Our coating facility utilizes non-acid mechanical grit blasting (Sa 2.5) for surface preparation, followed by immersion in non-electrolytic phosphating solutions and controlled post-bake thermal sintering cycles, reducing atomic hydrogen diffusion risks.
What information is required to receive an immediate quotation?
Please specify: 1) Fastener type and standard (e.g., ASME B18.2.1 heavy hex bolt, full thread stud bolt); 2) Substrate material grade (e.g., ASTM A193 B7, Inconel 718); 3) Coating specification (e.g., Whitford Xylan 1070 Blue over zinc phosphate); 4) Dimensions (diameter, thread pitch, overall length); 5) Quantity and project delivery timeline; and 6) Supplementary testing mandates (such as NACE MR0175 sour service or 3.2 inspection).

Request Technical Sourcing & Engineering Consultation

Connect with our applications engineering department to finalize coating selection, thread tolerance calculations, or to obtain immediate pricing for your international projects. Our team provides fast turnaround on detailed quotes and technical data packages.

Contact Us