
Tailored industrial bolting, full-thread bars, double-end engineered studs, and heavy-duty socket fasteners designed to meet exact ISO, ASTM, DIN, and project specifications.
A comprehensive engineering guide to mechanical integrity, thread formation methods, microstructural control, and metallurgical selection for severe operating environments.
Continuous OEM threaded rods fabricated via cold thread rolling display significantly higher fatigue life compared to cut threads. The roll-forming process plastically deforms the grain flow structure so that it continuously follows the thread contour without breaking fibers. This cold work induction creates residual compressive stresses at the thread roots, significantly improving resistance to fatigue crack propagation, notch sensitivity, and cyclic operational loads in vibrating marine and chemical pumping infrastructure.
When operating environments exceed the limits of austenitic stainless steels (such as 304 and 316L), custom OEM fabrication shifts to precipitation-hardenable superalloys. Our processing of Inconel 718 (UNS N07718), Hastelloy C276 (UNS N10276), and Super Duplex 32750 (UNS S32750) strictly controls gamma double-prime (γ″) precipitation strengthening and PREN ratings exceeding 42, ensuring absolute resistance against localized pitting, crevice erosion, and chloride-induced stress corrosion cracking (SCC).
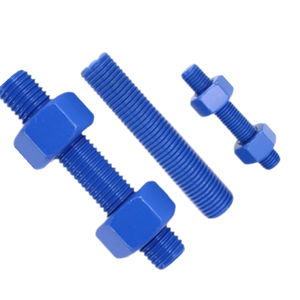
For high-pressure, subsea, and offshore flanged assemblies, friction coefficient consistency and galvanic isolation are mandatory. Our specialized fluoropolymer treatments (including Xylan blue PTFE), electro-deposited high-purity zinc coatings, and mechanical galvanizing are calibrated to achieve uniform film thicknesses without root-thread clogging. This guarantees torque tension repeatability, eliminates galling between identical stainless mating surfaces, and delivers up to 3,000+ hours of ASTM B117 salt spray endurance.
| Material Designation | UNS / Code | Yield Strength Min. (MPa) | Tensile Strength (MPa) | Corrosion Resistance / Service Envelope | Primary Industrial Compliance |
|---|---|---|---|---|---|
| Inconel 718 | UNS N07718 | 1,034 | 1,241 - 1,400 | High temp oxidation resistance up to 650°C; cryogenic to extreme thermal cycles | API 6A CRA, ASTM B637, NACE MR0175 |
| Hastelloy C276 | UNS N10276 | 355 | 790 - 850 | Immunity to wet chlorine gas, hypochlorite, and ferric/cupric chlorides | ASTM B574, ASME SB574, PED 2014/68/EU |
| Super Duplex 2507 | UNS S32750 | 550 | 750 - 1,000 | PREN ≥ 42; extreme resistance to marine chloride pitting and crevice erosion | ASTM A479, EN 10272, NORSOK M-650 |
| ASTM A193 B7 | AISI 4140/4142 | 725 | 860 - 1,000 | Chromium-molybdenum high tensile bolting for mid-to-high pressure vessels | ASME B16.5 Flange Bolting, ASTM A193 |
| Carbon Steel 12.9 | High Alloy Quenched | 1,100 | 1,220 - 1,300 | Extreme tensile loading, high static load structural fastening | ISO 898-1, DIN 912, DIN 976 OEM |
Strategic industry shifts, evolving regulatory requirements, and technical criteria modern procurement managers must integrate into global RFP frameworks.
Global mega-projects across Europe and North America increasingly disqualify fastener suppliers that cannot deliver end-to-end cryptographic or validated traceability. Threaded studs and continuous rods now require raw-melt heat number validation back to origin, chemical spectrum verification via OES/PMI, and digital EN 10204 3.1 or 3.2 documentation to mitigate counterfeit alloy risks in high-consequence operating zones.
Tighter environmental mandates under RoHS, REACH, and EPA are accelerating the phase-out of hexavalent chrome coatings and unregulated cadmium plating. Modern procurement specifications prioritize waterborne fluoropolymer matrices, zinc-nickel alloy electroplating, and ceramic-infused barrier layers that achieve salt-spray life exceeding 1,500 hours without the risk of hydrogen embrittlement in high-strength fasteners.
As the costs of critical alloying elements (Nickel, Molybdenum, Cobalt) fluctuate, lean manufacturing paradigms dictate less machining swarf waste. Tier-1 OEM fastener manufacturers utilize localized induction heating and precision near-net warm forging for large-diameter rods (>M36 or >1-1/2"), backed by cryogenic coolant-assisted CNC machining for superalloys like Inconel 718 to preserve optimal surface integrity.
Leveraging state-of-the-art production infrastructure, accredited metallurgy, and certified international management systems to support mission-critical installations worldwide.
Our administrative headquarters in Mumbai combined with our manufacturing plant in Rajkot, Gujarat, integrate cold heading, hot forging, high-speed multi-axis CNC lathes, and thread rolling under a single ISO 9001:2015 registered umbrella.
Fully certified to manufacture and supply pressurized bolting for European pressure vessel equipment. We verify metallurgical impact values, chemical compositions, and elongation metrics in full compliance with PED Annex I requirements.
Every exported threaded rod shipment is matched with mill test certificates guaranteeing 100% heat traceability. Inspection dossiers witnessed by DNV, Lloyd's Register, TÜV, or Bureau Veritas are regularly managed for offshore energy operators.
Preventing sulfide stress cracking (SSC) in sour gas environments is a cornerstone of our metallurgy. We provide controlled-hardness heat treatment, solution annealing, and Charpy V-notch toughness testing down to -196°C for LNG cryogenic hardware.
We maintain comprehensive master alloy stocks of Inconel (625, 718), Hastelloy (C276, B2), Monel 400, Titanium (Gr 2, Gr 5), Duplex 2205, and Super Duplex 2507 bar stock, drastically compressing lead times for custom machined OEM orders.
From heavy-duty wooden crating lined with moisture-barrier wrapping to ISPM-15 treated pallets, all goods are packed for safe air, ocean, and remote-site transport across Europe, North America, the Middle East, Southeast Asia, and Australia.
Direct answers to the most common engineering, compliance, tolerance, and documentation questions from piping engineers and procurement professionals.
Whether you require custom Inconel 718 full-thread rods for downhole wellheads, Hastelloy C276 studs for chemical reactors, or high-tensile 12.9 DIN976 bars, our senior metallurgical team is standing by to evaluate your project specifications.