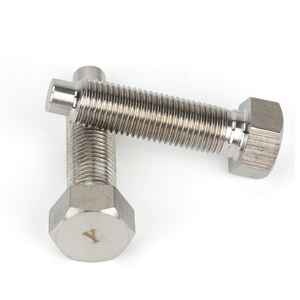
OEM Turbomachinery Bolting & Rotor Hardware

Custom OEM Turbine Fasteners Supplier & Exporter

Precision-engineered creep-resistant studs, casing bolts, rotor tie-rods, and diaphragm nuts built in superalloys and high-temperature grades under ISO 9001:2015 and PED 2014/68/EU certification.

750°C+

Continuous Creep-Rupture Threshold

100%

EN 10204 3.1 & 3.2 Heat Traceability

M12–M130

Hot Forged & Rolled Thread Diameters

0.02mm

Tight Precision Pitch & Flank Tolerances

Turbine Hardware Portfolio

High-Integrity Fasteners & Superalloy Fastening Systems

Explore our precision-manufactured fasteners designed for turbine diaphragms, steam chest casings, exhaust collectors, marine turbines, and high-temperature industrial skids. Engineered for zero thermal relaxation and extreme cyclical stress.
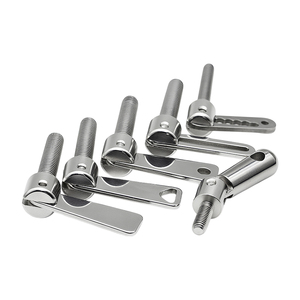
Stainless Steel L-Shaped Hand Twist Fasteners
Turbine Enclosure Hardware

Stainless Steel L Shaped Adjustable Hand Twist Screw Quick Release Corner Mount Bolt 1/4 M3-M10 Fishing Box Rod Holder Fastener

Alloy Grades: AISI 304, 316L, 17-4 PH Marine Application: Acoustic Enclosures, Shrouds & Quick Panels
View Product Specs
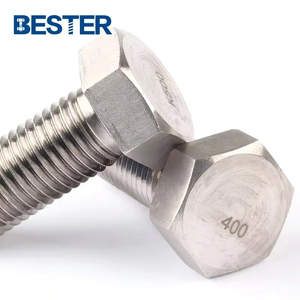
Monel 400 External Hexagon Extended Bolt
Marine Turbine Steam Lines

Monel400 Nickel-copper Alloy External Hexagon Bolt Extended Screw Rod British Standard 2.4360 High-strength Grade China

Alloy Grades: Monel 400 (UNS N04400), W.Nr. 2.4360 Application: Saltwater Steam Exhausts & Desalination Feed
View Product Specs
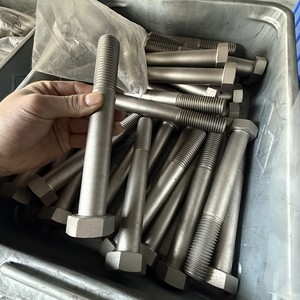
Monel 400 K-500 Heavy Hex Head Bolt
Heavy Structural Bolting

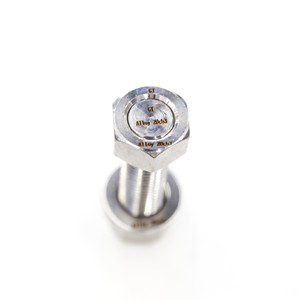
Custom High Tensile Plain Finish Monel 400 K-500 M20 Monel 400 Uns N04400 Alloy Heavy Hex Head Bolt

Alloy Grades: UNS N05500 (K-500), Age-Hardened Application: High-Torque Casing Joint Flanges & Pumps
View Product Specs
Incoloy 925 and Grade 321 Heavy Hex Hardware
Corrosion & Thermal Sets

Corrosion Resistant M42 ASME B18.2.3.1M F593 Grade 321 10.9 Incoloy 925 Stainless Steel Hex Head Nuts Bolts and Washers

Alloy Grades: Incoloy 925, AISI 321, ASTM F593 Application: High-Temperature Steam Valve Manifolds
View Product Specs
PTFE Fasteners Kit for Chemical Isolation
Dielectric & Chemical Seals

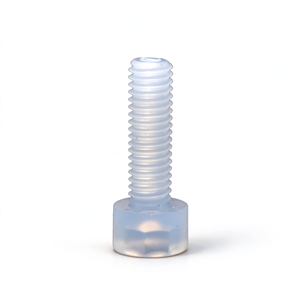
PTFE Plastic Fastener Assortment Kit High Temperature Non-Stick Screw Set for Chemical Industry

Material: Virgin PTFE / Modified Fluoropolymers Application: Galvanic Isolation & Acid Condensation Zones
View Product Specs
Stainless Steel 304 Double End Stud Bolts
Flange & Piping Connection

Stainless Steel 304 A2-70 DIN 976 M6-M30 Double End Stud Right Hand Thread for Flange Connection Pipeline Petrochemical Made

Standards: DIN 976, ASME B16.5, ASTM A193 B8 Application: High-Pressure Turbine Auxiliary Piping
View Product Specs
Hastelloy C276 Dog End Bolts
High-Temp Combustor Hardware

High Temperature Alloy Corrosion-Resistant C276 Nickel Alloy Hexagon Hex Head Dog End Bolts

Alloy Grades: Hastelloy C-276 (UNS N10276), 2.4819 Application: Gas Turbine Transition Liners & Combustors
View Product Specs
PTFE Coated High Performance Bolts
Low-Friction Anti-Galling Studs

Fasteners High Performance Hexagon Head Bolts PTFE Coated Steel Stainless Steel Thread OEM Custom Cut Dimensions Tools Hardware

Coating Type: Multi-Layer Xylan® / PTFE Fluoropolymer Application: Repeat Torquing on Turbine Casings
View Product Specs
Metallurgical Whitepaper

Turbomachinery Bolting Architecture: Creep, Relaxation & Fatigue

Turbine bolting represents the apex of mechanical fastener engineering. Operating under high internal steam pressures (up to 300 bar) and gas combustion temperatures exceeding 650°C, turbine bolts undergo continuous elastic strain relaxation, requiring specialized metallurgical compositions to maintain joint integrity without catastrophic stress rupture.

Continuous Grain Flow Forging

Unlike standard machined fasteners that sever the natural microstructure of bar stock, our turbine casing studs and heavy bolts are manufactured via precision hot heading and warm forging. This aligns the metallic grain flow continuously through the head-to-shank transition radius, slashing notch sensitivity and delivering up to 40% higher cyclic fatigue endurance under extreme rotor vibrations.

Stress Relaxation Resistance

Over thousands of operational hours, turbine studs lose elastic clamp load due to high-temperature creep. By employing age-hardenable superalloys such as Inconel 718 (UNS N07718), Nimonic 80A, and ASTM A453 Grade 660, our fasteners exhibit negligible stress relaxation up to 700°C, preventing dangerous steam bypass and flange leakage between scheduled turbine overhauls.

Anti-Galling & Thread Rolling

Superalloys possess intense work-hardening tendencies that lead to immediate thread galling during breakout. We eliminate this failure mode by utilizing post-heat-treatment thread rolling to generate ultra-smooth root radii with burnished surface finishes down to Ra 0.4 µm, complemented by micro-layer silver, molybdenum disulfide, or high-temperature PTFE dry-film coatings.

Engineering Specification Guide

Turbine Alloy Selection Matrix: Mechanical & Thermal Properties

A rigorous comparative analysis of standardized exotic alloy bolting materials utilized across heavy-duty industrial gas turbines, supercritical steam installations, and offshore aeroderivative units.

Material Grade UNS / DIN Norm Max Operating Temp Yield Strength (0.2%) Tensile Strength (Rm) Primary Turbine Functional Zone
Inconel 718 UNS N07718 / 2.4668 650°C (1200°F) ≥ 1,034 MPa ≥ 1,240 MPa Gas Turbine Rotor Discs, Combustor Shells, Tie-Bolts
A453 Gr. 660 (A286) UNS S66286 / 1.4980 540°C (1000°F) ≥ 585 MPa ≥ 895 MPa Steam Turbine Cylinder Casings & Intermediate Piping
Nimonic 80A UNS N07080 / 2.4952 750°C (1382°F) ≥ 620 MPa ≥ 1,000 MPa Extreme Supercritical Steam Casings & Valve Stems
Hastelloy C-276 UNS N10276 / 2.4819 450°C (842°F) ≥ 355 MPa ≥ 790 MPa Flue Gas Desulfurization (FGD) Skids & Sour Waste Turbines
Monel K-500 UNS N05500 / 2.4375 480°C (896°F) ≥ 790 MPa ≥ 1,100 MPa Marine Propulsion Turbines & Offshore Seawater Pumps
ASTM A193 B16 Cr-Mo-V Alloy Steel 538°C (1000°F) ≥ 725 MPa ≥ 860 MPa HP Steam Chest Valves & Steam Generator Manifolds
Super Duplex 2507 UNS S32750 / 1.4410 280°C (536°F) ≥ 550 MPa ≥ 750 MPa Offshore Wind Turbine Subsea Tower Foundation Bolting
The OEM Advantage

Engineering Precision, Global Compliance & Export Scale

Combining our centralized trading and engineering office in Mumbai with high-capacity forging and CNC machining operations in Rajkot, India, TorqBolt Inc. delivers uncompromising reliability for global turbomachinery and critical infrastructure installations.

State-of-the-Art Manufacturing Capabilities

We operate a fully integrated production ecosystem tailored to rapid prototyping, customized small-batch turbine development, and high-volume framework supply agreements.

Hot Forging Line Presses up to 1,200 Tons
CNC Turning Centers Multi-Axis Mazak & Doosan
Thread Rolling Diameters up to M130 (5")
In-House Heat Treat Atmospheric Solution & Aging
  • Complete Heat Traceability: Every bolt, nut, and stud is marked with indelible heat numbers correlating to raw ingot melt logs.
  • Custom Geometries to OEM Blueprints: Precision casing bolts with central bore holes for electric heating rods during bolt tensioning.
  • Zero Defect Philosophy: 100% optical dimensional inspection and ultrasonic testing (UT) per ASTM A388 for subsea and turbine rotating assemblies.

International Accreditations & Quality Rigor

Our quality control infrastructure is certified by global third-party notified bodies, guaranteeing compliance with European, American, and international pressure codes.

Quality Standard ISO 9001:2015 Registered
Pressure Directives PED 2014/68/EU (TÜV Rheinland)
Material Certificates EN 10204 Type 3.1 & 3.2
Sour Service NACE MR0175 / ISO 15156
  • Third-Party Witnessing: Regular inspection coordination with DNV, Lloyd's Register, Bureau Veritas, and TÜV.
  • Metallurgical Laboratory: In-house Charpy V-notch impact testing down to -196°C, tensile testing up to 1,200 kN, and micro-Vickers hardness verification.
  • Global Export Packaging: Anti-corrosive VCI vacuum sealing, heavy-duty wooden crating, and direct expedited courier or sea container forwarding.
Procurement & Technical FAQ

Frequently Asked Questions on Turbine Fastener Procurement

Engineered answers addressing critical material, dimensioning, inspection, and commercial criteria for procurement managers and mechanical integrity specialists.

What makes turbine fasteners distinct from standard ASTM petrochemical bolting?
+
Standard piping fasteners (such as ASTM A193 B7 or B8) are designed for static pressure containment at moderate temperatures. Turbine bolting operates in active dynamic environments characterized by intense cyclic fatigue, high-speed thermal transients, and stress-relaxation conditions above 550°C. Turbine fasteners feature custom shank-to-head fillet radii, gun-drilled centers for elongation measurement or internal heating rods, rolled threads performed after final heat treatment, and specialized superalloys (Inconel 718, Nimonic 80A, A453 Gr. 660) to prevent joint opening caused by creep relaxation.
How does TorqBolt ensure thread galling prevention on superalloy fasteners?
+
Galling occurs when friction and pressure break through the passive oxide layer of stainless steels and nickel alloys, resulting in micro-welding of mating threads. We eliminate galling through three technical protocols: (1) Cold thread rolling rather than single-point cutting, resulting in a mirror-like finish (Ra ≤ 0.4 µm) with compressive residual surface stresses; (2) Controlled differential hardness between the stud/bolt and mating nut (typically maintaining a 30–50 HB hardness differential); and (3) Application of engineered surface treatments such as silver plating (AMS 2410), high-bake MoS2, or PTFE fluoropolymer coatings that sustain lubrication up to extreme assembly torques.
Can TorqBolt manufacture turbine studs directly to proprietary OEM drawings?
+
Yes. A significant portion of our business involves custom OEM replacements and reverse-engineered parts matching legacy turbine designs (including Siemens, GE, Alstom, Mitsubishi, and Westinghouse designs). Our multi-axis CNC machines and custom tooling allow us to manufacture necked-down (waisted) shank studs, dog-end alignment bolts, taper-shank bolts, and multi-piece castle nut assemblies in full conformance with proprietary engineering drawings, metric, UNC, UNF, or 8UN thread pitches.
What documentation and non-destructive testing (NDT) are supplied per shipment?
+
Every shipment is accompanied by a certified EN 10204 Type 3.1 inspection report detailing full chemical composition (heat-level analysis), room temperature and elevated-temperature tensile test results, yield point, elongation, reduction of area, Charpy V-notch impact values, and brinell/rockwell hardness. On demand, we provide EN 10204 Type 3.2 certificates witnessed by independent agencies (DNV, TÜV, Lloyd's, BV). Optional NDT includes 100% Wet Magnetic Particle Inspection (MPI) or Liquid Penetrant Inspection (LPI) on threads and heads, Ultrasonic Examination (UT) per ASTM A388, and Positive Material Identification (PMI) by portable XRF analyzer.
How do you manage lead times for exotic raw materials like Inconel 718 or Hastelloy?
+
To prevent project downtime, we maintain extensive safety stocks of prime European and Indian mill-certified round bars in diameters ranging from 12mm to 120mm across key grades: Inconel 718, Inconel 625, Hastelloy C-276, Monel 400/K-500, Duplex 2205, Super Duplex 2507, 17-4 PH, and A453 Grade 660. For standard sizes and urgent turnaround needs, finished fasteners can be produced and delivered via express airfreight within 10–15 business days.

Connect with Our Turbomachinery Fastening Engineers

Have an upcoming turbine turnaround, planned maintenance outage, or new OEM turbine skid development? Submit your dimensional drawings, alloy grades, and testing criteria directly to our senior metallurgy and procurement desk.

Contact Us