Engineered directly from hot-forged bar, cold-headed stock, and precision CNC turning cells under stringent ISO 9001:2015 and PED 2014/68/EU quality controls.
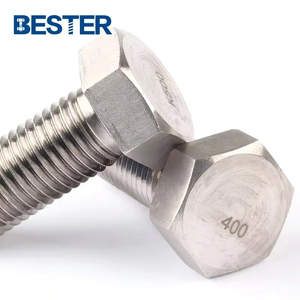
A 25% Cr super duplex stainless steel with deliberate additions of tungsten (W) and copper (Cu), delivering remarkable resistance to localized pitting, crevice erosion, and stress corrosion cracking (SCC) in halide environments.
%Cr + 3.3(%Mo + 0.5%W) + 16(%N) confirms exceptional localized pitting immunity.
More than double the proof stress of conventional AISI 316L austenitic bolting.
Tested at -46°C (-50°F) to verify absence of brittle sigma or chi phase precipitates.
Tight ferrite-austenite phase balance strictly verified per ASTM E562.
| Elemental & Mechanical Property | UNS S32760 (Zeron 100 / EN 1.4501) | UNS S32750 (2507 / EN 1.4410) | UNS S31803 / S32205 (Duplex 2205) | Compliance Standards |
|---|---|---|---|---|
| Chemical Composition (%) | Cr: 24.0-26.0 | Mo: 3.0-4.0 | Ni: 6.0-8.0 W: 0.50-1.00 | Cu: 0.50-1.00 | N: 0.20-0.30 |
Cr: 24.0-26.0 | Mo: 3.0-5.0 | Ni: 6.0-8.0 W: - | Cu: 0.50 max | N: 0.24-0.32 |
Cr: 21.0-23.0 | Mo: 2.5-3.5 | Ni: 4.5-6.5 W: - | Cu: - | N: 0.08-0.20 |
ASTM A276, ASTM A479, ASME SA-479 |
| PREN Formula Index | ≥ 42.0 [PREN = %Cr + 3.3(%Mo+0.5%W) + 16%N] | ≥ 41.0 [PREN = %Cr + 3.3%Mo + 16%N] | ≥ 34.0 [PREN = %Cr + 3.3%Mo + 16%N] | Norsok M-650 / ISO 15156-3 |
| 0.2% Proof Stress (Rp0.2) | ≥ 550 MPa (80 ksi) | ≥ 550 MPa (80 ksi) | ≥ 450 MPa (65 ksi) | ASTM A182 (Grade F55), ASTM A1082 |
| Tensile Strength (Rm) | 750 - 1000 MPa (109 - 145 ksi) | 750 - 1000 MPa (109 - 145 ksi) | 655 - 880 MPa (95 - 128 ksi) | EN ISO 3506-1 (Grade A4/A5) |
| Critical Pitting Temp (CPT) | ≥ 45°C - 50°C | ≥ 42.5°C - 47.5°C | ≥ 30°C - 35°C | ASTM G48 Method C / Method E |
| Sour Gas Service Limit | Max 28 HRC per ISO 15156 / NACE MR0175 | Max 28 HRC per ISO 15156 / NACE MR0175 | Max 28 HRC per ISO 15156 / NACE MR0175 | NACE MR0175 / ISO 15156-3 Annex B |
A rigorous evaluation based on metallurgy qualifications, NORSOK M-650 validation, hot-forging tool control, thread rolling capability, in-house laboratory testing, and international project execution.
Premier specialty fastener manufacturer operating comprehensive hot-forging, CNC machining, and cold heading lines. Recognized globally for fast-track production of UNS S32760 / F55 stud bolts, heavy hex nuts, and bespoke flange bolting certified to PED 2014/68/EU and Norsok MDS D57.
Established European manufacturer specializing in high-integrity bolting for North Sea offshore installations. Offers deep inventory of fully certified super duplex and alloy steel bar stock with hot-forging capability up to M100.
Over a century of experience supplying safety-critical fasteners to nuclear, energy, and petrochemical EPC contractors. State-of-the-art heat-treatment facilities ensuring zero intermetallic sigma precipitation in UNS S32760.
Major regional bolting manufacturer catering to GCC offshore operators (Aramco, ADNOC, QatarEnergy). Holds massive stocks of F55 blanks and fully threaded studs with in-house Xylan and PTFE coating booths.
World leaders in multi-jackbolt tensioning systems. Produces custom UNS S32760 tensioner nuts and high-tensile structural mechanical pre-load devices engineered specifically for vibrating offshore compressor stations.
Specializes in precision-engineered specialty screws, fasteners, and custom drawings in super duplex alloys. Serves European pharmaceutical, wastewater, and marine desalination plant skid builders.
One of North America's largest integrated manufacturers of bolting and industrial sealing gaskets. Comprehensive super duplex stud production adhering strictly to ASME B16.5 and B16.47 piping flange classes.
Pioneers in high-volume, cold-forged stainless and duplex fasteners for Scandinavian heavy marine and renewable offshore wind turbine turbine sub-structures requiring dynamic shear resistance.
Top Italian forged fastener producer supplying European offshore valve, pump, and pressure vessel OEMs with fully certified Grade F55 / 1.4501 hot-forged socket screws, eye bolts, and double-end studs.
Renowned worldwide stockholder and manufacturer of exotic piping products, maintaining designated super duplex bolting production lines for FPSO topsides, seawater cooling loops, and subsea risers.
Market dynamics, raw material hedging, and stringent QA traceability are transforming how global engineering contractors source super duplex bolting.
Global operators are discontinuing intermediary broker sourcing in favor of manufacturers offering 100% heat-number digital trace back to European or Indian melt mills. Complete digital trace via EN 10204 3.1 & 3.2 guarantees raw billet chemistry, ferrite ratios, and prevents counterfeit alloy dumping.
While austenitic 316L bolts possess lower purchase costs, premature failure due to chloride stress corrosion cracking (CSCC) induces catastrophic shutdown expenses. Specifying UNS S32760 delivers a 35-year design lifespan with zero corrosion-related downtime in offshore seawater spray zones.
With prolonged 20-30 week production windows from Western European manufacturers, engineering firms are actively rerouting capital bolting contracts to Tier-1 Indian manufacturing hubs like Rajkot and Mumbai that combine Western pedigree metallurgical certifications with rapid 4-6 week production cycles.
How cutting-edge hot-forging, thread rolling, and barrier nanocoatings are eliminating microstructural embrittlement and galling issues in super duplex bolting.
Super duplex UNS S32760 possesses a very narrow hot-working window (1000°C - 1180°C). Heating outside this range precipitates deleterious intermetallic phases such as sigma (σ) and chi (χ) that ruin impact toughness. Modern computerized induction forging coupled with millisecond water quenching preserves clean, ductile grain flow through the critical bolt head-to-shank transition radius.
Traditional cut threads tear structural fibers and generate micro-notches susceptible to fatigue cracking under cyclic offshore current loading. Advanced manufacturing mandates cylindrical die thread rolling after solution annealing. This cold-work process burnishes the root radius, induces beneficial compressive residual stresses, and doubles fatigue endurance.
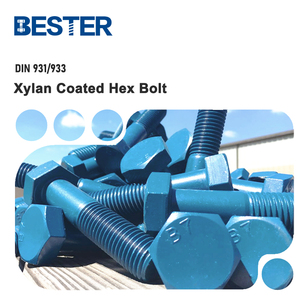
Super duplex alloys are notorious for severe galling during pneumatic high-torque torquing. Factories now apply thin-film PTFE Xylan 1424 / 1070 and ceramic fluoropolymers over zinc phosphate undercoats. This provides an exact nut-factor coefficient of friction (μ = 0.08-0.12), ensuring precise bolt stretch without costly galling seizure in field assembly.
Direct metallurgical answers addressing compliance, quality control standards, and subsea failure prevention.
While both are super duplex grades with ~25% Chromium and PREN ≥ 40, UNS S32760 contains deliberate additions of 0.5-1.0% Tungsten (W) and 0.5-1.0% Copper (Cu). Tungsten markedly improves resistance to localized pitting in low-pH chloride solutions, while copper provides exceptional corrosion resistance in non-oxidizing mineral acids like sulfuric and hydrochloric acid environments.
Yes. Under NACE MR0175 / ISO 15156-3 (Table A.24), UNS S32760 is qualified for sour service environments provided it is supplied in the solution-annealed condition with a maximum hardness of 28 HRC (271 HBW) and a ferrite content between 35% and 65%. TorqBolt conducts 100% calibrated Rockwell hardness testing on every manufacturing heat lot.
Super duplex steels are prone to rapid precipitation of intermetallic sigma (σ) and chi (χ) phases between 600°C and 900°C. Even microscopic traces of sigma phase destroy low-temperature toughness without necessarily altering tensile strength. A Charpy impact test value ≥ 80 Joules (single) / 60 Joules (average) at -46°C verifies a microstructurally clean material structure per ASTM A923 Method B.
Each delivery should include a certified EN 10204 3.1 inspection certificate (or 3.2 witnessed by third parties such as Lloyd's Register, DNV, or Bureau Veritas). Essential recorded data includes melt heat number, chemical composition (% W and Cu), tensile and yield stress, elongation, reduction of area, Charpy impact toughness at -46°C, ASTM G48 Method A ferric chloride pitting test results (zero pitting at 50°C), and phase balance analysis.
Caution is critical. Under high cathodic over-protection (potentials more negative than -1050 mV vs Ag/AgCl), super duplex steels are vulnerable to Hydrogen-Induced Stress Cracking (HISC) if yield stresses are excessive. Fastener designs must adhere strictly to DNVGL-RP-F112 guidelines with controlled hardness levels (≤ 28 HRC) and strict cold-work limits.
Stud bolts are fabricated to ASME B18.31.2 / ASTM A193 Grade B8M/B8R or custom drawing classes. Heavy hex nuts are manufactured per ASME B18.2.2 or ISO 4033, utilizing UNS S32760 / ASTM A194 Grade 8M/Grade 6. Hex head bolts adhere to ASME B18.2.1, DIN 931 (partial thread), DIN 933 (full thread), and ISO 4014 / 4017.
Founded in 2010, TorqBolt Inc. has grown from an Indian manufacturing powerhouse into an internationally accredited partner for Tier-1 EPC contractors, offshore yards, and pump-valve manufacturers worldwide. Headquartered in Mumbai with advanced production mills in Rajkot, Gujarat, we maintain in-house control over forging, CNC thread rolling, heat-treatment solution annealing, and non-destructive examination (NDE).
Whether your inquiry involves urgent replacement studs for an offshore manifold shutdown or heavy M36-M90 super duplex anchor rods, our technical sales engineers will calculate thread stresses, recommend anti-galling coatings (Xylan/PTFE), and provide an all-inclusive technical quotation within hours.