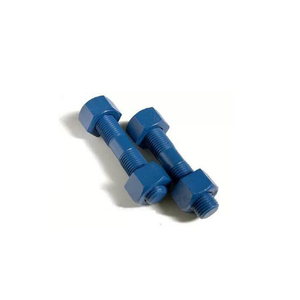

In response to the extreme thermal dynamics, high stress concentrations, and aggressive chloride environments across the Norwegian Continental Shelf (NCS) and industrial fjords, our enterprise delivers premium-grade Nimonic 80A (UNS N07080 / 2.4952) forged fasteners. Combining precision Chinese metallurgy with international compliance auditing, we supply critical infrastructure projects from Stavanger to Hammerfest.
Explore our certified bolting array manufactured under rigid quality controls via hot forging, cold heading, and precision CNC threading.
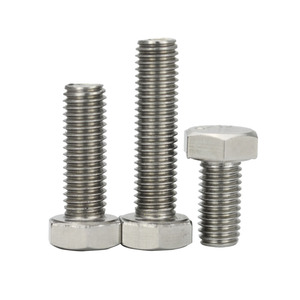
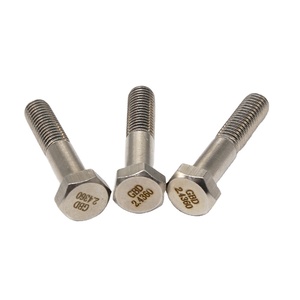
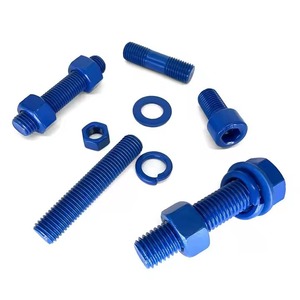
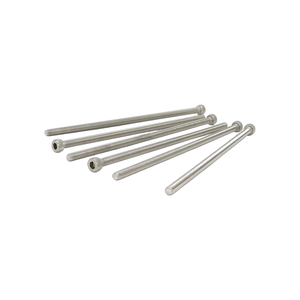
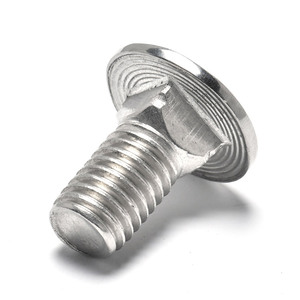
Nimonic 80A is a wrought, age-hardenable nickel-chromium alloy strengthened by additions of titanium and aluminium, creating gamma prime (γ') precipitates. Designed primarily for sustained load-bearing capacity under severe service temperatures up to 815°C (1500°F).
| Alloy Element / Property | Nominal Content (%) / Test Method | Technical Function in High-Stress Nordic Marine Environments |
|---|---|---|
| Nickel (Ni) | Balance (~65.0 - 71.0%) | Matrix stabilization; eliminates chloride stress corrosion cracking (CSCC) found in standard austenitics. |
| Chromium (Cr) | 18.0 - 21.0% | Forms a protective self-healing Cr2O3 oxide film; guards against high-temperature sulfur and oxidation attack. |
| Titanium (Ti) | 1.80 - 2.70% | Primary constituent in forming intermetallic Ni3(Ti, Al) gamma prime phases that impede dislocation motion. |
| Aluminium (Al) | 1.00 - 1.80% | Secondary gamma prime constituent; provides exceptional thermal creep resistance and sustained yield integrity. |
| Carbon (C) & Boron (B) | C: 0.04-0.10% | B: ≤ 0.008% | Carbide precipitation along grain boundaries inhibits grain boundary sliding during extended thermal cycling. |
| Tensile Strength (Rm) | ≥ 1,000 - 1,250 MPa | Ensures high-clamping force capability under extreme mechanical pressures in subsea valves and gas turbomachinery. |
| Yield Strength (Rp 0.2) | ≥ 620 - 780 MPa | Prevents micro-plastic deformation during thermal shock cycles and critical flange torque operations. |
The industrial landscape of Norway represents one of the most demanding engineering testing grounds in the world. Sourcing Nimonic 80A fasteners from our manufacturing facility provides local engineering procurement contractors (EPCs) with the precise structural resilience required.
Installed on floating production storage and offloading units (FPSOs) and subsea manifolds operating in the Ekofisk, Johan Sverdrup, and Troll fields. Resists both deep-sea cathodic embrittlement and high-pressure steam valve degradation where conventional super duplex grades exceed thermal limits.
Equinor and associated energy facilities operate high-efficiency aeroderivative gas turbines. Nimonic 80A hex-head bolts, exhaust studs, and nozzle clamping components sustain extreme centrifugal stress and thermal shock cycles without stress relaxation.
Norwegian fjord environmental regulations (IMO Tier III and national zero-emission maritime directives) demand scrubbers handling concentrated acidic wash-water and hot exhaust gas condensates where Alloy 80A hardware provides dependable service longevity.
The transition of Norway's industrial matrix from conventional petroleum extraction toward high-efficiency offshore wind, hydrogen conversion, and carbon capture drives new structural requirements for superalloy bolting.
Projects such as Northern Lights (Longship) require compression systems cycling at cryogenic-to-high thermal ranges under dense supercritical CO2 phase changes. Nimonic 80A fasteners avoid embrittlement during cyclic pressure-relief operations.
With deep offshore sites like Utsira Nord and Sørlige Nordsjø II, pitch-bearing structural fasteners experience high cyclic fatigue and marine salt-fog exposure. Superalloy fastening mitigates costly offshore maintenance campaigns.
Norwegian engineering operators are shifting away from lower initial material capital expenditure (CapEx) in favor of OpEx containment. Replacing recurring duplex fastener maintenance with age-hardened Nimonic 80A reduces lifecycle inspection costs.
Combining domestic specialty raw material supply lines with stringent European testing protocols, our direct factory model delivers certified quality with reliable supply schedules.
Operating under rigorous ISO 9001:2015 and PED 2014/68/EU guidelines validated by TUV Rheinland. We regularly accommodate EN 10204 3.2 third-party inspections (DNV, Lloyd's Register, Bureau Veritas).
Our closed-die hot forging processes preserve continuous grain boundaries along the critical head-to-shank fillet transition, significantly improving fatigue life compared to standard machined bolts.
Automated two-stage thermal processing: solution annealing at 1080°C followed by controlled precipitation aging at 700°C for 16 hours to ensure homogeneous gamma-prime development.
Fasteners are sealed in moisture-barrier VCI bags and heavy-duty ISPM-15 heat-treated maritime plywood crates to endure North Atlantic and Arctic ocean shipping routes without surface oxidation.
Direct answers addressing technical compliance, documentation standards, and logistical workflows for importing to Norway.
Connect with our metallurgists and international export engineers. Submit your technical drawings, material grades, or project specifications to receive a formal quotation complete with full certification breakdowns.
Get a Quote