
Manufactured using hot induction forging, cryogenic thread rolling, and precision 5-axis CNC machining. Every fastener undergoes rigorous magnetic particle, ultrasonic, and hydrostatic testing to guarantee zero failure under cyclic fatigue, thermal surges, and aggressive chemical exposure.
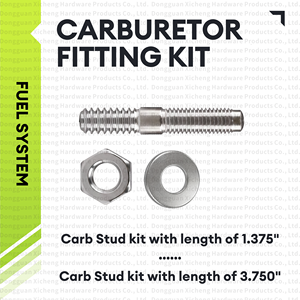
Engineered for extreme manifold pressures and intense thermal cycles. Features rolled threads to eliminate notch stress, offering superior resistance against volatile hydrocarbons and high-pressure fuel vapors.
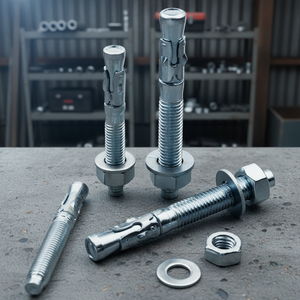
Heavy-duty structural wedge anchor engineered to secure high-pressure piping brackets, hydraulic skids, and compressor bases against severe seismic shear and dynamic mechanical pulsation.
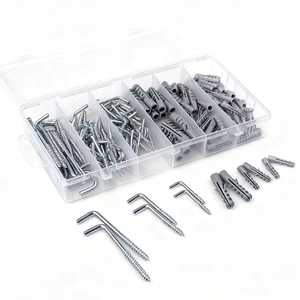
Precision friction-grip concrete plug anchors for mounting pneumatic service manifolds, hydraulic trace heating lines, and secondary pressure instrument panels within factory floors.
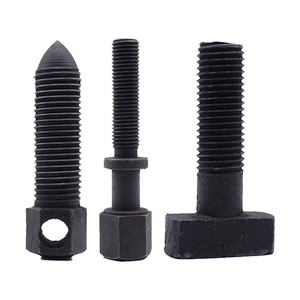
Drawing-customized T-head and hammer-head bolts produced on Multi-Axis turning centers. Tailored for clamping high-pressure autoclave lids, heavy press guides, and turbine housing assemblies.
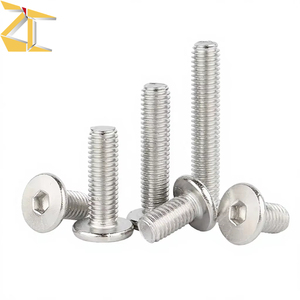
Engineered for cleanroom robotic valves, pneumatic manifolds, and micro-fluidic actuators in semiconductor lithography tooling where clearance is tight and zero fluid leakage is non-negotiable.
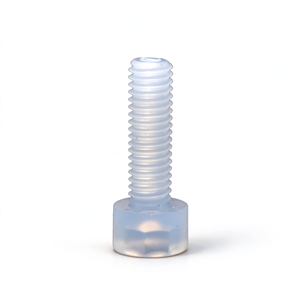
Pure virgin polytetrafluoroethylene threaded fasteners providing ultimate dielectric isolation and total chemical non-reactivity in electro-pickling tanks, wet chemical benches, and acid lines.
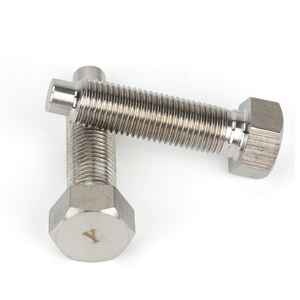
Hastelloy C276 bolting engineered specifically for sour-gas (H2S), flue gas desulfurization, and wet chlorine scrubbers. Features a unthreaded dog-end guide to speed up flange alignment under high torque.
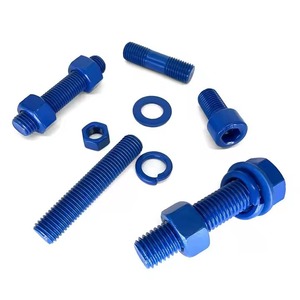
The global benchmark for pressure boundary piping. AISI 4140 alloy steel quenched and tempered to ASTM A193 Class B7, paired with continuous fluoropolymer (Xylan 1070) coating to ensure uniform torque breakout.
In high-pressure systems exceeding 20 MPa (2,900 PSI) and reaching up to 150 MPa (21,750 PSI), fastener integrity governs overall process safety. Bolted joint failure in high-pressure gas or hydraulic service originates from micro-yielding, hydrogen embrittlement, stress-corrosion cracking (SCC), or thread stripping under cyclic impulse fatigue.
Unlike machined bar bolts whose load-bearing thread grains are severed during cutting, our hot-headed and cold-formed bolts retain uninterrupted fibrous crystalline orientation along the head-to-shank radius. This dramatically suppresses fatigue notch sensitivity under pulsating hydraulic and acoustic line frequencies.
Threads are rolled post-heat treatment under severe hydrostatic compression. This work-hardens thread roots, generating intense compressive residual stresses that prevent micro-crack initiation even under thermal shock cycles spanning -196°C (cryogenic LNG service) to +550°C (steam turbine extraction lines).
Gall-prone exotic alloys like UNS S32750 (Super Duplex) and Inconel 718 undergo specialized dry-film molybdenum disulfide (MoS2) or multi-coat fluoropolymer (PTFE / Xylan) bonding. This achieves an extremely stable nut friction coefficient (μ = 0.10 - 0.14), ensuring exact hydraulic tensioning bolt preload.
The Greater Tokyo Megalopolis encompasses Japan's dense concentration of precision chemical facilities, heavy power generation, semiconductor research clusters, and port infrastructure. Our high-pressure bolting directly addresses the stringent engineering demands of the Kanto industrial belt.
Installed across fluid catalytic cracking units (FCCUs) and hydrogen desulfurization reactors where operational pressures hit 15 to 22 MPa at 450°C. ASTM A193 B16, B7, and Incoloy 825 heavy hex bolts withstand sour gas (H2S), high partial hydrogen pressure, and polythionic acid stress cracking.
Tokyo Bay LNG terminals process millions of tons of liquefied natural gas annually. Our ASTM A320 Grade L7, L7M, and austenitic B8M Class 2 stud bolts guarantee full Charpy V-notch impact toughness below -196°C, preventing brittle fracture in high-pressure submerged boil-off pumps and transfer arms.
The Metropolitan Area Outer Underground Discharge Channel utilizes high-capacity hydraulic flood drainage pumps operating under violent subterranean hydrostatic back-pressures. High-tensile DIN standard wedge anchors and stainless expansion bolts secure hydraulic conduits against cavitation.
Tokyo leads Japan's Green Transformation (GX) with 700-bar fuel cell bus and passenger car corridors. Fasteners in these hydrogen compressors demand zero susceptibility to hydrogen-induced embrittlement. We supply vacuum-melted A-286 (UNS S66286) and Strain-Hardened 316L fasteners fully compliant with JARI S001 standards.
Precision fab toolmakers and research labs across West Tokyo require miniature low-profile socket cap screws in 304/316L and virgin PTFE fasteners for toxic silane, arsine, and ultra-high purity nitrogen gas delivery manifolds requiring helium leak tightness under 10 MPa supply pressures.
High-speed rail rolling stock traversing Tokyo Station, Shinagawa, and Ueno utilizes our precision CNC machined hammer head and shear bolts inside electro-pneumatic braking actuators that sustain constant dynamic vibration and sudden pressure surges.
Comprehensive metallurgical data comparing yield strength, operating temperature thresholds, corrosion resistance numbers (PREN), and international pressure vessel design code equivalents.
| Alloy Grade | UNS / Material No. | Yield Strength Min. (MPa) | Tensile Strength Min. (MPa) | Max Pressure Class | Temp. Limits (°C) | Standards Equivalents |
|---|---|---|---|---|---|---|
| ASTM A193 B7 | AISI 4140 / G41400 | 725 MPa (105 ksi) | 860 MPa (125 ksi) | ASME Class 2500 | -29°C to +427°C | JIS SCM440 EN 42CrMo4 |
| ASTM A193 B16 | Chromium-Moly-Vanadium | 725 MPa (105 ksi) | 860 MPa (125 ksi) | Superheated Steam | -29°C to +538°C | DIN 40CrMoV4-6 |
| Inconel 718 | UNS N07718 / 2.4668 | 1,034 MPa (150 ksi) | 1,275 MPa (185 ksi) | API 15,000+ PSI | -250°C to +650°C | API 6A CRA NACE MR0175 |
| Hastelloy C276 | UNS N10276 / 2.4819 | 355 MPa (51 ksi) | 790 MPa (115 ksi) | Severe Chemical Press. | -196°C to +400°C | ASTM B574 JIS NW 0276 |
| Super Duplex 2507 | UNS S32750 / 1.4410 | 550 MPa (80 ksi) | 750 - 1000 MPa | ASME Class 2500 Subsea | -50°C to +250°C | EN 10272 NORSOK M-650 |
| Stainless 316L (A4-80) | UNS S31603 / 1.4404 | 600 MPa (Strain Hard) | 800 MPa | ASME Class 900 | -196°C to +300°C | JIS SUS316L ISO 3506-1 |
| Titanium Grade 5 | UNS R56400 (Ti-6Al-4V) | 828 MPa (120 ksi) | 895 MPa (130 ksi) | Hyperbaric Subsea | -250°C to +400°C | ASTM B348 JIS H4600 |
Procuring high-pressure bolting components within Japan has shifted beyond baseline catalog dimensions. Tokyo-based engineering contractors (EPCs) and plant operators now mandate holistic lifecycle compliance, stringent hydrogen compatibility, and dual-certified material integrity.
Under Japan's Ministry of Economy, Trade and Industry (METI) High Pressure Gas Safety Act (KHK), any piping element or pressure vessel operating above 1.0 MPa (compressed gases) or 0.2 MPa (liquefied gases) must have traceable Mill Inspection Certificates verifying impact energy values and chemical limits.
Following updated seismic codes for Tokyo Bay chemical complexes, bolting must not fail in shear during severe lateral ground acceleration. Fasteners now integrate controlled ductile zones with mandatory elongation (≥16%) and strict Charpy V-notch toughness to absorb cyclic shock.
Global Japanese EPCs executing international turnkey energy projects require fasteners dual-certified to American specifications (ASME Section VIII, B16.5, ASTM A193) and Japanese Industrial Standards (JIS B 1180, JIS B 1186, JIS B 0205) to ensure frictionless inspection clearance.
Operating under integrated ISO 9001:2015 and European Pressure Equipment Directive (PED 2014/68/EU) certified by TÜV Rheinland, we bridge the gap between heavy industrial forging and micron-level precision CNC machining.
Direct logistical corridors to Haneda (HND), Narita (NRT), and the Port of Tokyo. We handle export documentation, customs carnets, and express courier logistics for urgent plant shutdown turnarounds within the Keihin complex.
Every lot is tied to its originating melt heat. Mechanical tensile, yield, elongation, reduction of area, Charpy impact at cryogenic temperatures, and Positive Material Identification (XRF & OES) are documented under 3.1 or 3.2 inspection with third-party witness (Lloyd's, DNV, BV).
Need non-standard dog ends, hammer-head profiles, ultra-fine pitches, or internal pressure tapping ports? Our multi-axis CNC turn-mill machining centers execute drawing-based geometries from single-piece prototypes to high-volume production batches.
Key technical answers regarding METI regulations, material certificates, cryogenic testing, and ordering logistics for high-pressure bolting.
Our fasteners are manufactured using certified raw material heats from audited mills. Under METI regulations, high-pressure equipment bolting requires verifiable mechanical strength, chemical composition, and heat treatment logs. We supply comprehensive EN 10204 3.1 inspection documentation (with 3.2 third-party verification upon request) containing complete chemical analysis, tensile testing, 0.2% proof stress, and Charpy impact data satisfying KHK inspector audits.
Yes. Many Japanese EPC firms design plants combining ASME B16.5 flange pressure classes with domestic JIS pipe fabrication. We routinely dual-certify fastener materials—such as cross-certifying ASTM A193 Grade B7 with JIS SCM440, and ASTM A193 B8M with JIS SUS316. Threading can be executed in Unified Inch (UNC, UNF, 8UN) or Metric coarse/fine pitch per JIS B 0205.
Stainless steel, Super Duplex, and Inconel threads are prone to severe galling (cold welding) under the high torques required for pressure boundary seals. We offer PTFE fluorocarbon coatings (Xylan 1070/1424), baked MoS2 (Molybdenum Disulfide) dry lubricant, electrolytic silver plating for high-temperature turbine casings (up to 700°C), and micro-thin zinc-nickel plating with trivalent passivation.
Standard stocked alloy lines (ASTM A193 B7, B8, B8M, A194 2H nuts) can be dispatched within 48 to 72 hours via express air cargo directly to Tokyo Narita (NRT) or Tokyo Haneda (HND), reaching plant sites in 4 to 6 business days. Custom forged or CNC machined exotic alloy orders (Inconel 718, Hastelloy C276, Super Duplex) generally carry a lead time of 2 to 3 weeks depending on raw material bar stock availability and heat treatment requirements.
Yes. Fasteners intended for sour service (containing hydrogen sulfide H2S) are heat-treated with strict hardness capping (e.g., maximum 22 HRC for ASTM A193 Grade B7M, or tailored solution annealing and precipitation hardening for Inconel 718 and Duplex grades). Hardness testing is conducted across both surface and core cross-sections to prevent Sulfide Stress Cracking (SSC).
Our comprehensive testing program includes 100% Positive Material Identification (PMI via handheld XRF analyzer), Magnetic Particle Inspection (MPI) for ferromagnetic alloys, Liquid Penetrant Inspection (LPI) for non-magnetic austenitic and nickel alloys, Ultrasonic Flaw Testing (UT) for large diameter bar stock, and Optical Comparator / Thread Pitch Micro-Gauging.
Whether you require standard ASTM A193 B7/B16 stud bolt sets for a refinery turnaround or custom-machined Hastelloy C276 and Inconel 718 bolts for severe hyperbaric containment, our engineering and metallographic team is ready to evaluate your bill of materials.