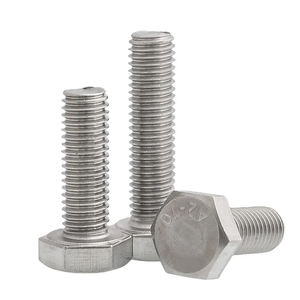
Precision hot-forged and CNC-machined studs, heavy hex bolts, and engineered clamping components supplied directly from our ISO 9001:2015 production facility to Riyadh infrastructure projects.
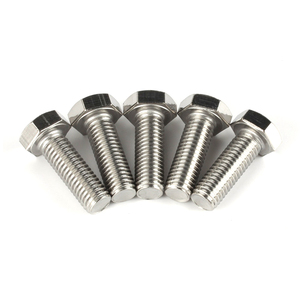
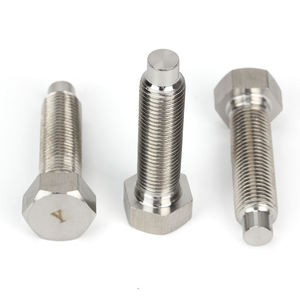
As operating temperatures in power plants and petrochemical furnaces in the Riyadh region push beyond 600°C, conventional austenitic stainless steels (316L, 321H) and standard Cr-Mo alloy steels (ASTM A193 B7/B16) undergo aggressive stress relaxation, microstructural spheroidization, and premature creep rupture. Nimonic 80A is an exceptional nickel-chromium precipitation-hardenable superalloy specifically formulated for critical load-bearing service up to 815°C (1500°F).
By precipitating coherent intermetallic gamma-prime [γ′ - Ni3(Al, Ti)] phases throughout an austenitic face-centered cubic matrix during a strictly controlled two-stage thermal cycle, Nimonic 80A fasteners exhibit sustained yield strength, exceptional rupture ductility, and unrivaled fatigue endurance under severe cyclic thermal gradients.
TorqBolt manufactures precision Nimonic 80A stud bolts, double-ended studs, heavy hex nuts, and turbine head bolts in full accordance with ASTM B637 UNS N07080, BS 3076 (HR1), and DIN EN 10269 (Material 2.4952 / 2.4631). Every production batch is backed by comprehensive 3.1 chemical and mechanical inspection protocols, ensuring flawless compliance with Saudi Aramco and Saudi Electricity Company (SEC) technical specifications.
Compare critical physical parameters and design limitations between Nimonic 80A and alternative alloy bolting specifications utilized in Saudi Arabian plants:
| Alloy Grade | UNS / DIN Mat. | Yield Strength 0.2% (MPa) | Tensile Strength (MPa) | Max Service Temp (°C) | Creep Rupture Strength (100h @ 700°C) | Primary Riyadh Application Target |
|---|---|---|---|---|---|---|
| Nimonic 80A | UNS N07080 / 2.4952 | ≥ 620 – 780 | ≥ 1,000 – 1,150 | 815 °C | ~370 MPa | Turbine exhaust, combustion chamber, catalyst crackers |
| Inconel 718 | UNS N07718 / 2.4668 | ≥ 1,030 | ≥ 1,240 | 650 °C | Rapid drop >650°C (phase instability) | Subsea wellheads, HP compressor casings |
| Incoloy A286 (660) | UNS S66286 / 1.4980 | ≥ 585 | ≥ 895 | 700 °C | ~210 MPa | Medium-temp manifold, turbocharger flanges |
| ASTM A193 B16 | Cr-Mo-V Alloy | ≥ 585 | ≥ 725 | 540 °C | Unusable >550°C due to scaling | Secondary steam lines, low-pressure piping |
| Hastelloy C276 | UNS N10276 / 2.4819 | ≥ 355 | ≥ 790 | 450 °C (Mechanical) | Non-precipitation hardened | Acid injection, wet chlorine, sour scrubbers |
Riyadh's harsh hyper-arid desert climate exposes thermal mechanical infrastructure to 50°C+ ambient summer temperatures, fine abrasive airborne silica, and intense thermal cycling during day-night swings.
Combined-cycle gas turbines (CCGT) powering Riyadh generate massive exhaust duct temperatures exceeding 650°C. Nimonic 80A studs secure transition pieces, turbine casing split lines, and fuel nozzle retaining rings against vibration-induced relaxation.
Hydrotreating reactors, atmospheric distillation heaters, and sulfur recovery units (SRU) demand high-nickel bolting immune to polythionic acid stress corrosion cracking and hydrogen embrittlement in severe sour gas service.
Thermal booster pumps and high-pressure steam distribution headers transporting desalinated water across the Najd plateau require corrosion-resistant, high-modulus fastener hardware capable of handling thermal water hammer.
High-pressure specialty petrochemical, polymer extrusion, and pharmaceutical synthesis plants operating in Riyadh's industrial hubs utilize Alloy 80A bolts on high-pressure autoclave reactors and heat exchanger tube sheets.
Large-scale centrifugal chillers and thermal storage units under King Abdullah Financial District utilize high-tensile alloy fasteners for critical condenser headers that withstand vibration without loosening.
Mainline gas turbine drivers at pump stations supplying crude oil through the Central Province rely on Nimonic 80A combustion hardware for round-the-clock uninterrupted throughput under severe desert sandstorm conditions.
How capital infrastructure expansion in the Kingdom is transforming high-temperature superalloy fastener specifications.
To reduce carbon intensity under the Saudi Green Initiative, Riyadh power generators are retrofitting gas turbines to accommodate natural gas-hydrogen fuel blends. Hydrogen combustion yields significantly higher flame temperatures and localized moisture, rapidly deteriorating standard 718 alloys and escalating demand for Nimonic 80A fasteners.
Saudi Aramco's In-Kingdom Total Value Add (IKTVA) framework and Royal Commission mandates require absolute transparency in material origins. Riyadh procurement departments are eliminating tier-3 trading intermediaries in favor of direct, accredited factory suppliers possessing verifiable in-house mill test certifications to EN 10204 3.1/3.2.
Shutdown turnaround timelines at Riyadh refinery and petrochem installations have tightened from 45 days down to sub-25 days. Supply chain success hinges on pre-machined, staged superalloy fastener packages delivered through King Khalid International Airport (RUH) bonded freight routes with immediate customs release.
Operating world-class hot forging, precision CNC turning, and in-house heat treatment facilities in Rajkot and corporate offices in Mumbai, TorqBolt bridges precision engineering with reliable Middle East delivery.
Certified by TÜV Rheinland for pressure-retaining equipment manufacturing. Fully audited for high-temperature critical bolting under European Pressure Equipment Directive standards.
Complete traceability from certified virgin billet to finished bolt. Independent third-party inspection agency (TPI) witnessing by SGS, DNV, Lloyd's Register, or Bureau Veritas available upon contract.
Grain flow is preserved through controlled induction heating and hot upsetting. Threads are cold rolled after precipitation hardening to generate severe compressive residual stresses, preventing dynamic shear fatigue.
Strict Rockwell C hardness testing (≤35 HRC or application specific) alongside microstructure metallography ensures no stress-sulfide cracking in Riyadh refinery gas treating units.
Our technical sales engineering team provides instant material feasibility, dimension checking to ASME/DIN, and DDP Riyadh logistics scheduling.
Every heat of Nimonic 80A undergoes seven rigorous gates of quality assurance prior to packaging and dispatch.
Optical Emission Spectrometry (OES) and Positive Material Identification (XRF) verify Ni, Cr, Ti, and Al chemistry against ASTM B637 UNS N07080.
Heads are formed at monitored temperatures (1050°C–1120°C) to guarantee unbroken grain flow at the critical head-to-shank junction.
Vacuum solution treatment at 1080°C followed by 16-hour precipitation aging at 700°C to yield optimum γ′ phase particle size distribution.
Threads are precision rolled between hardened dies, maintaining thread root radiuses in compliance with UNJ and Metric MJ aerospace profiles.
Practical answers to documentation, customs compliance, material substitution, and technical specifications for Saudi Arabian projects.
Our technical sales engineering team provides instant material feasibility, dimension checking to ASME/DIN, and DDP Riyadh logistics scheduling.